METALWORK

The Division
Everything Else
Is Built On

Aluminium is unforgiving. It conducts heat away faster than steel, so a weld that looks sound can be cold; it moves as it cools, so a frame that measured true in the fixture can leave it out of square; and it shows every ripple once a gloss coat goes over the top.

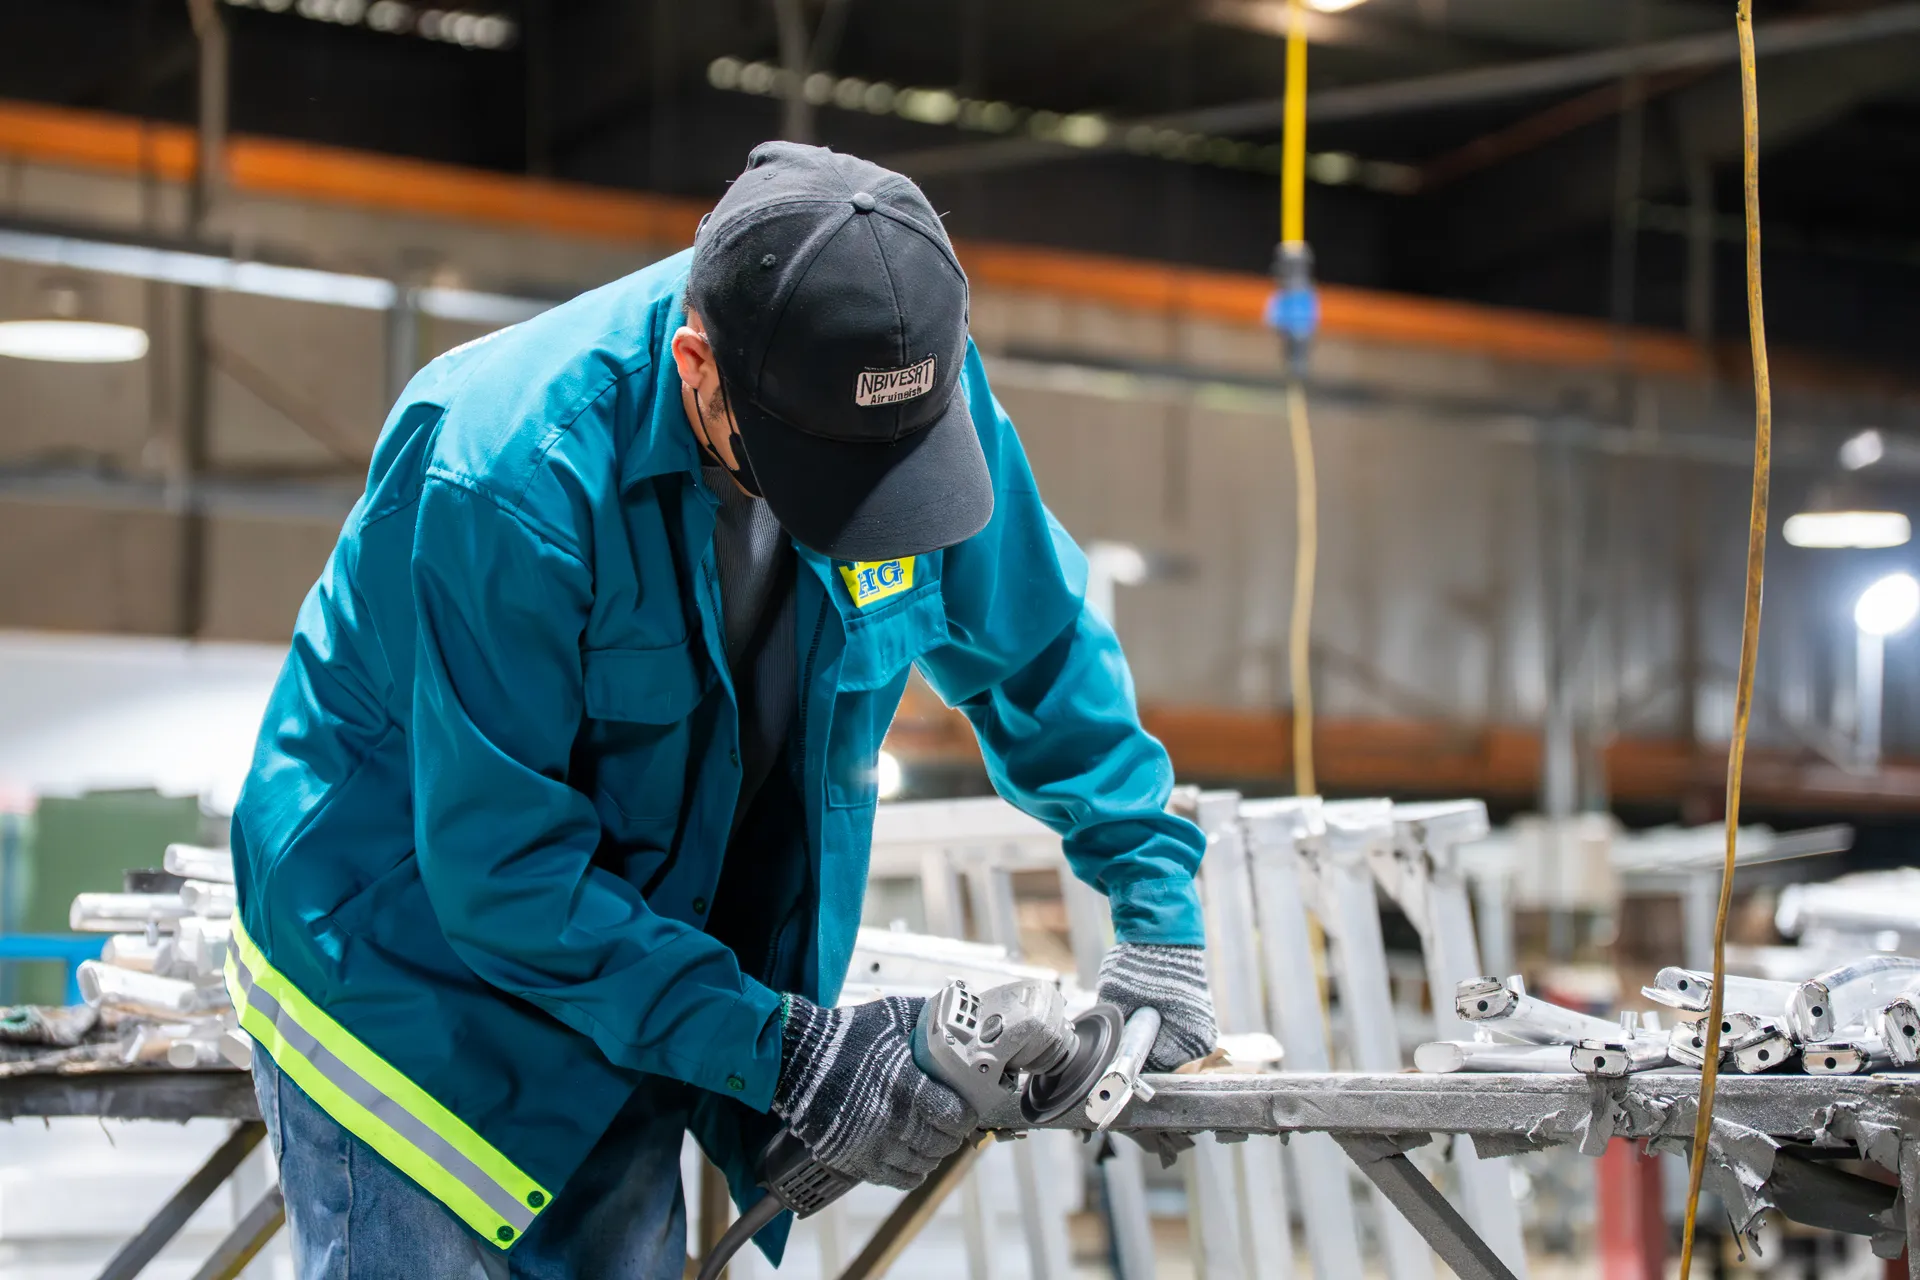
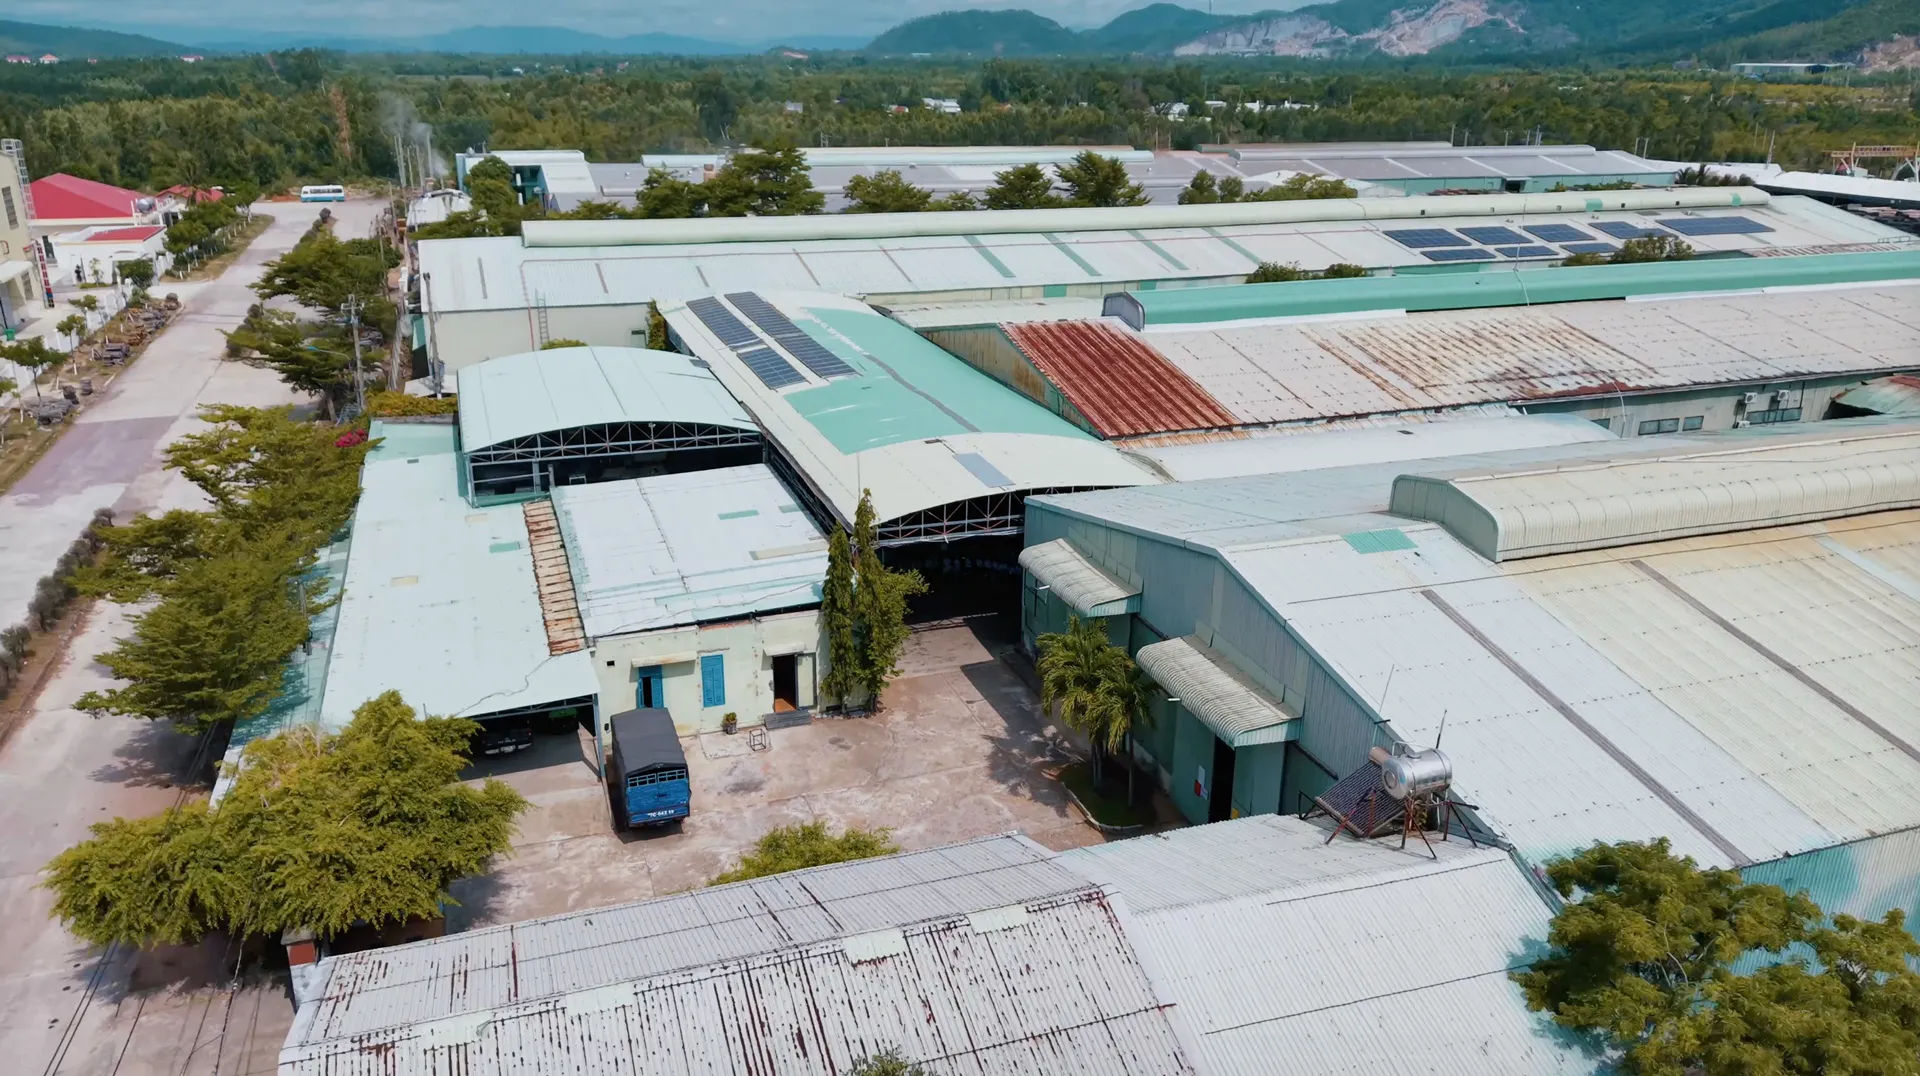
Our Mechanical Division is staffed with craftsmen who have spent years on the precise fabrication of steel, aluminium and stainless frames. The processes below are ordinary; holding them together across a long run is not.
THE CHAIN

Seven Steps From Billet
To Coated Frame

Section Design

Per programme

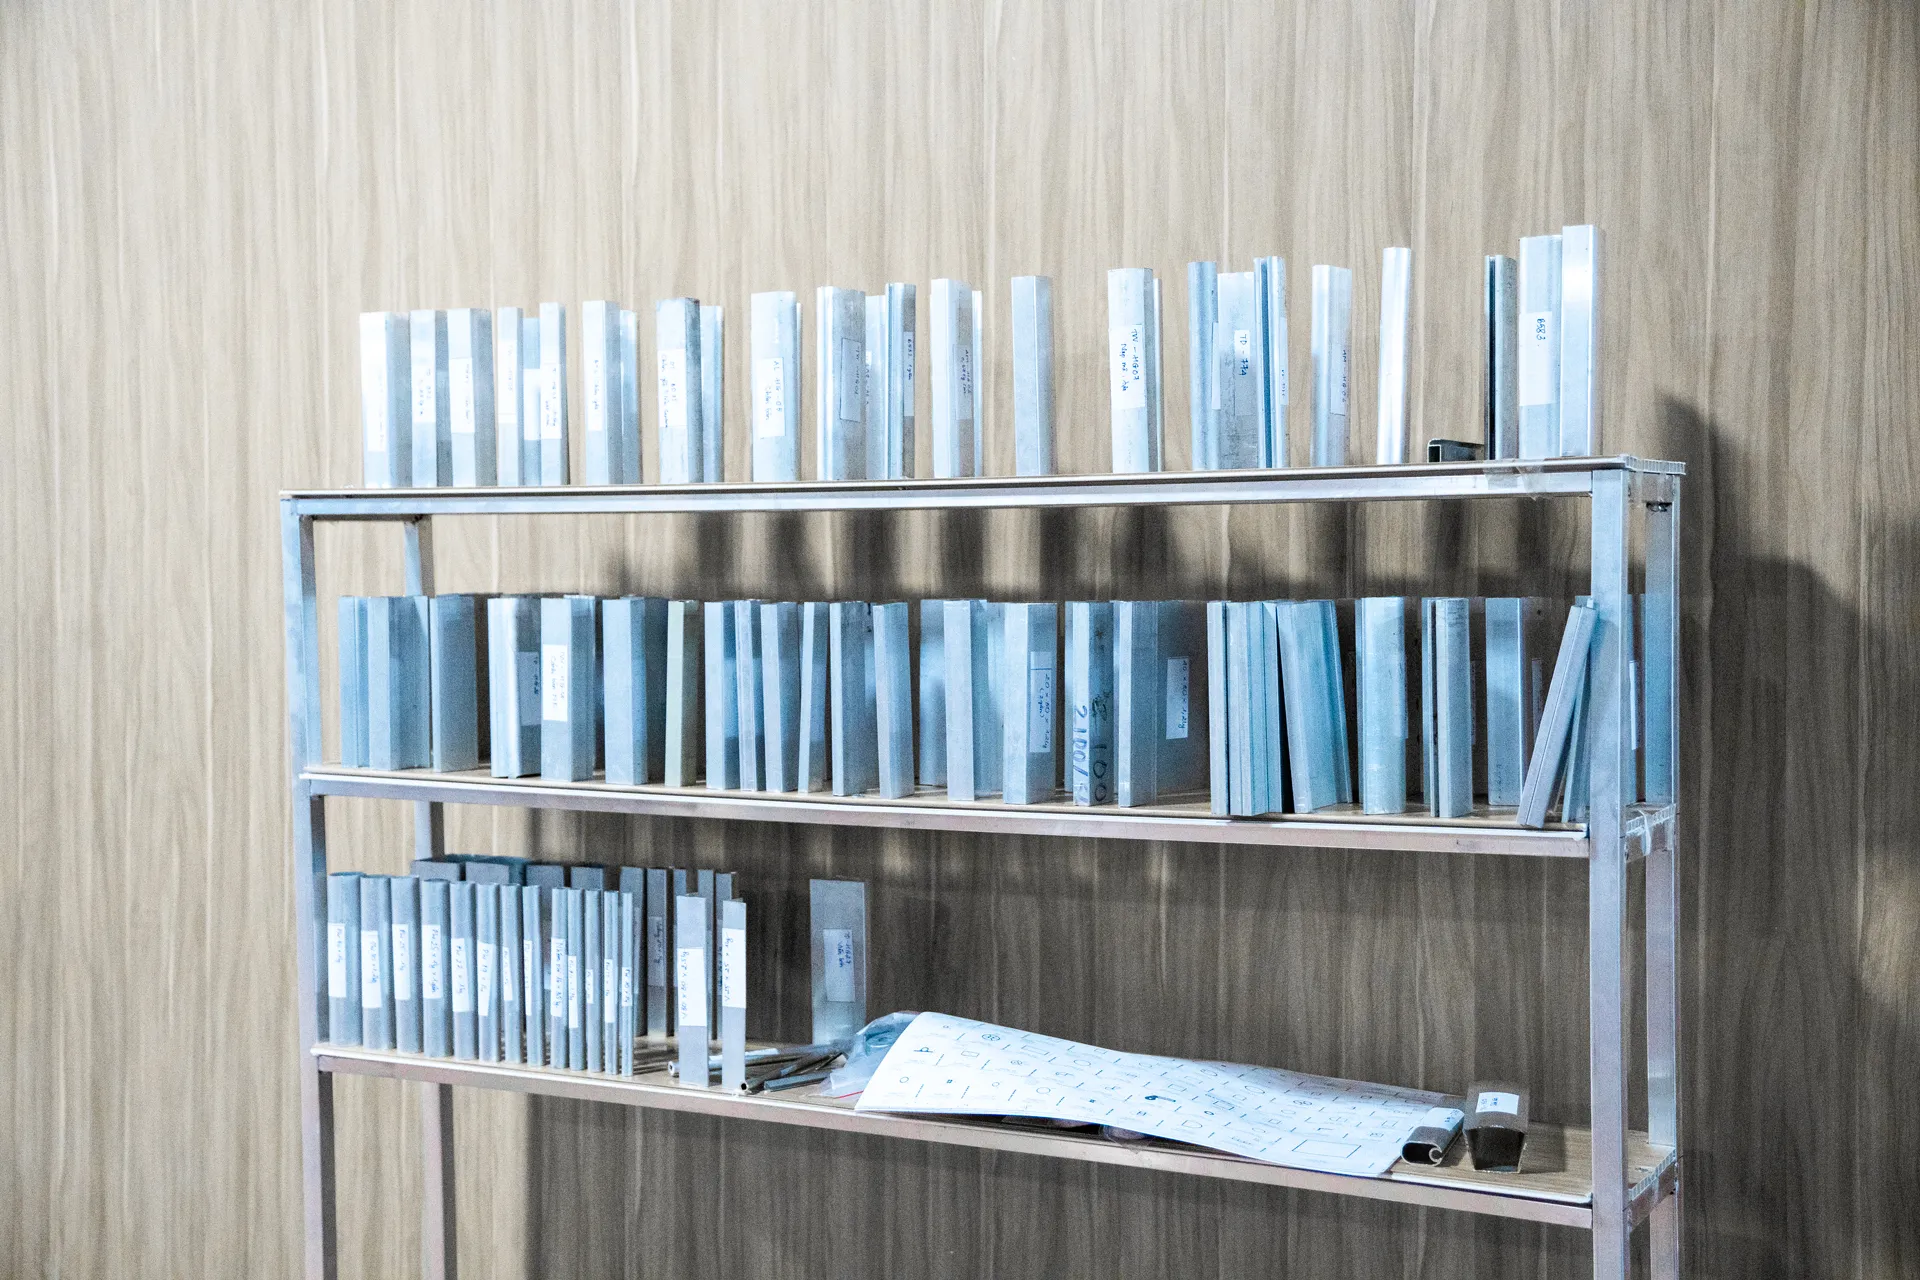
We draw our own extrusion profiles rather than buying stock tube. Wall thickness sits where the load is, and fixing points are extruded in rather than welded on — fewer welds, less distortion, a cleaner line.

Alloy & Certification

Per batch

6063-T5 as standard for frames, higher-strength alloys where a section is doing structural work. Every delivery arrives with a mill certificate and is verified before it enters the store.

Laser Cutting

±0.2 mm

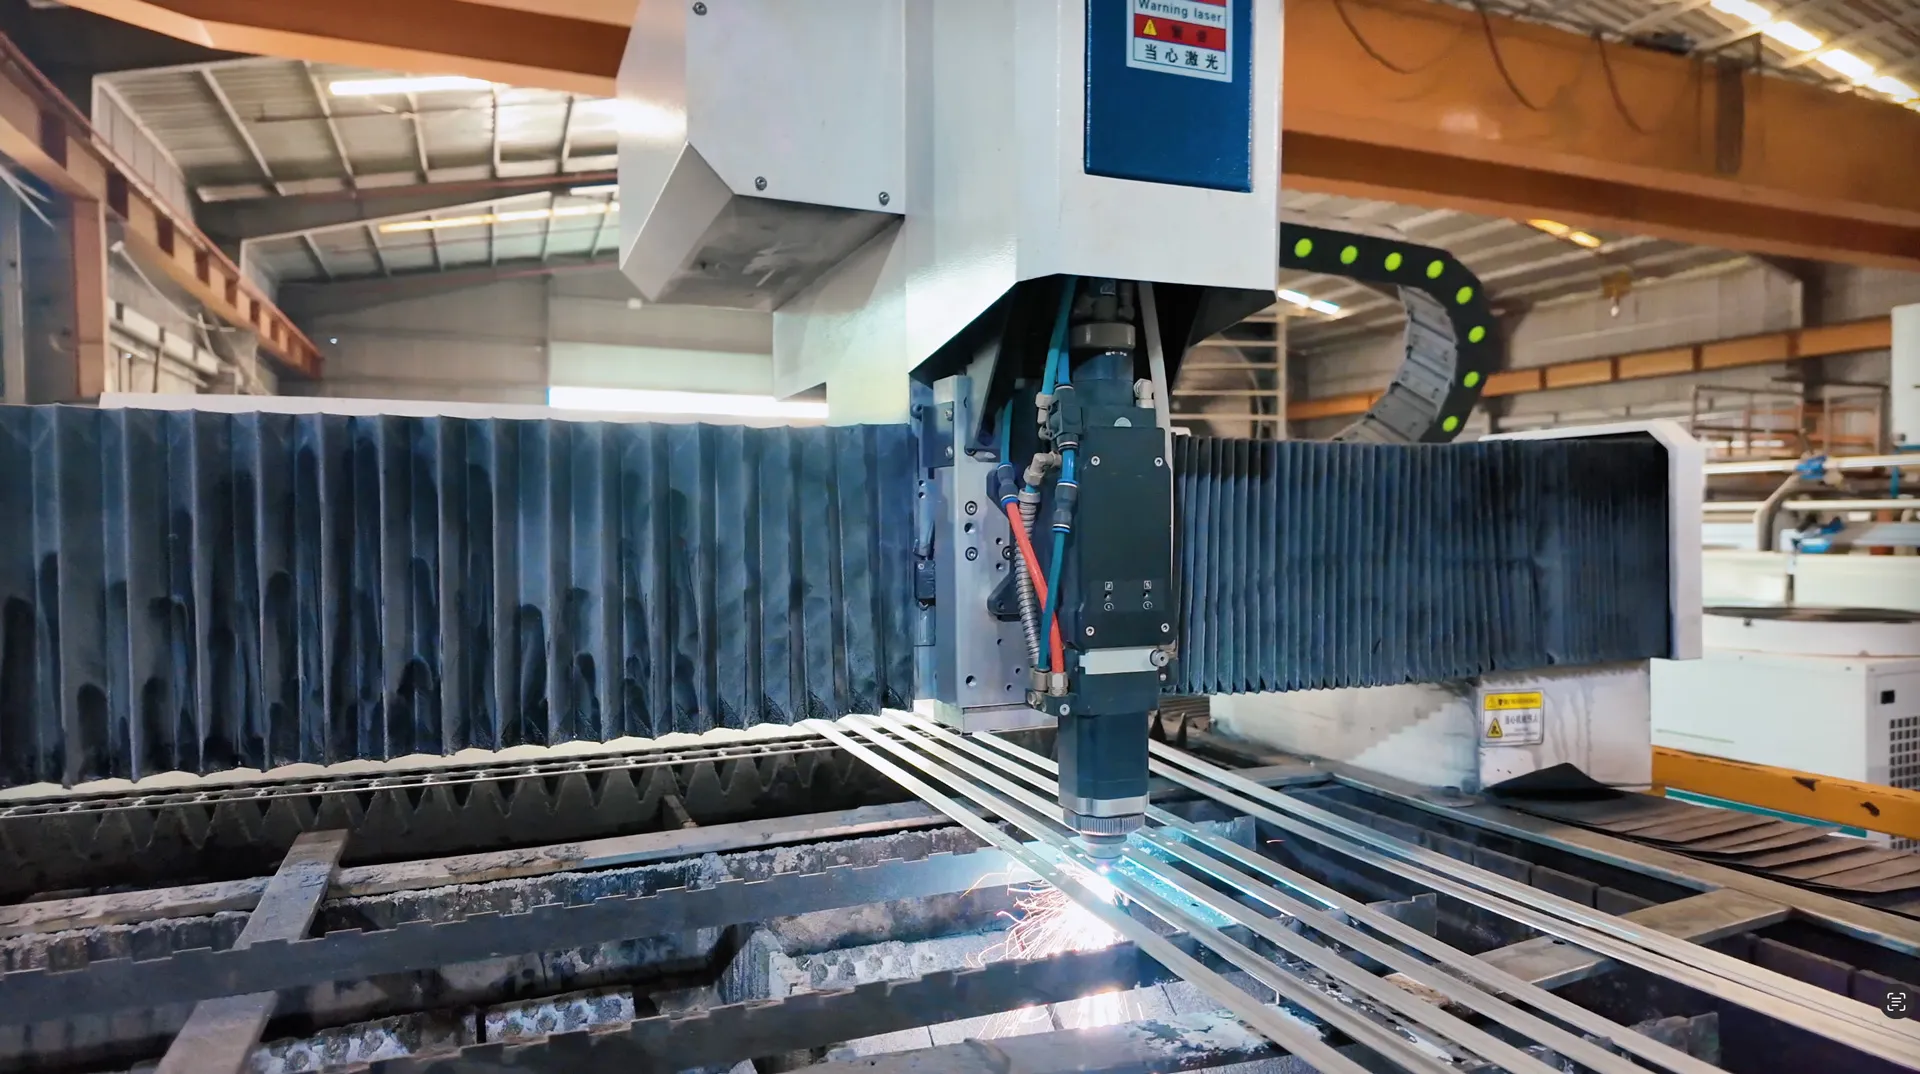
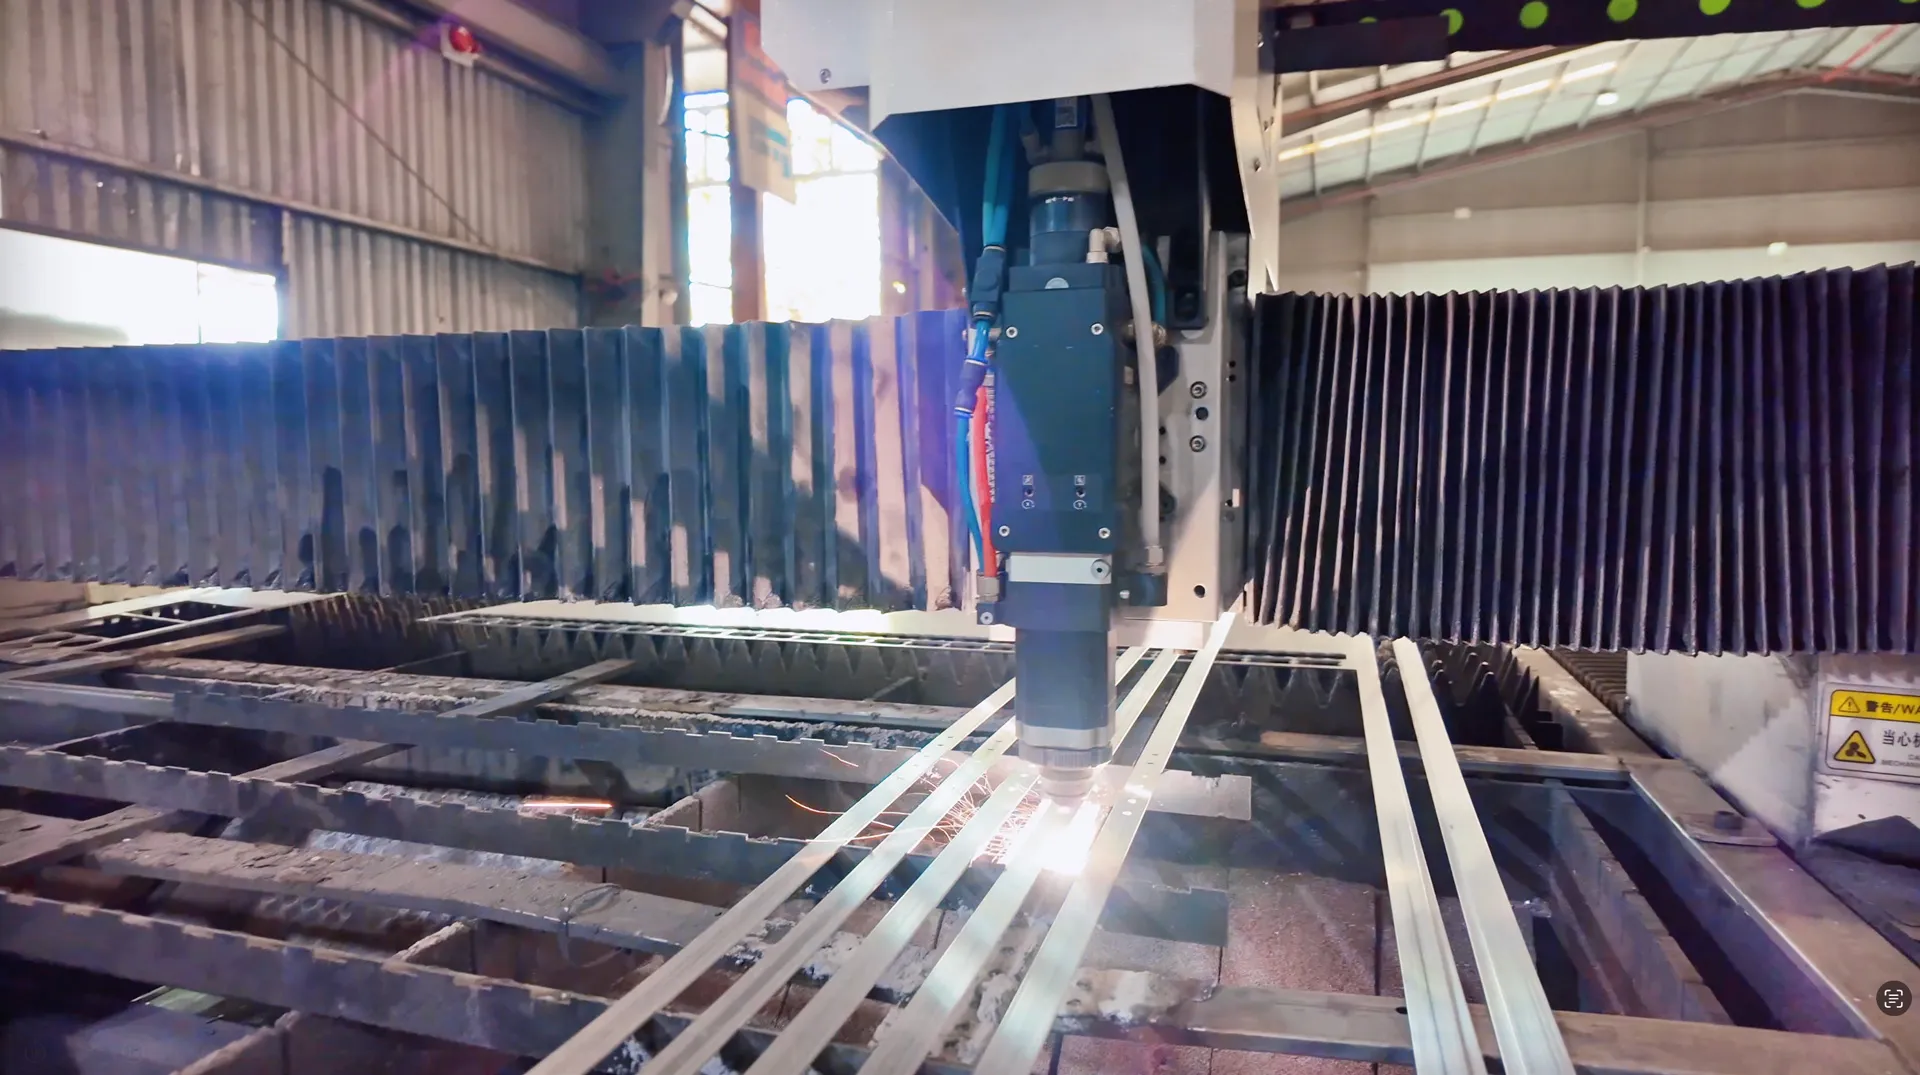
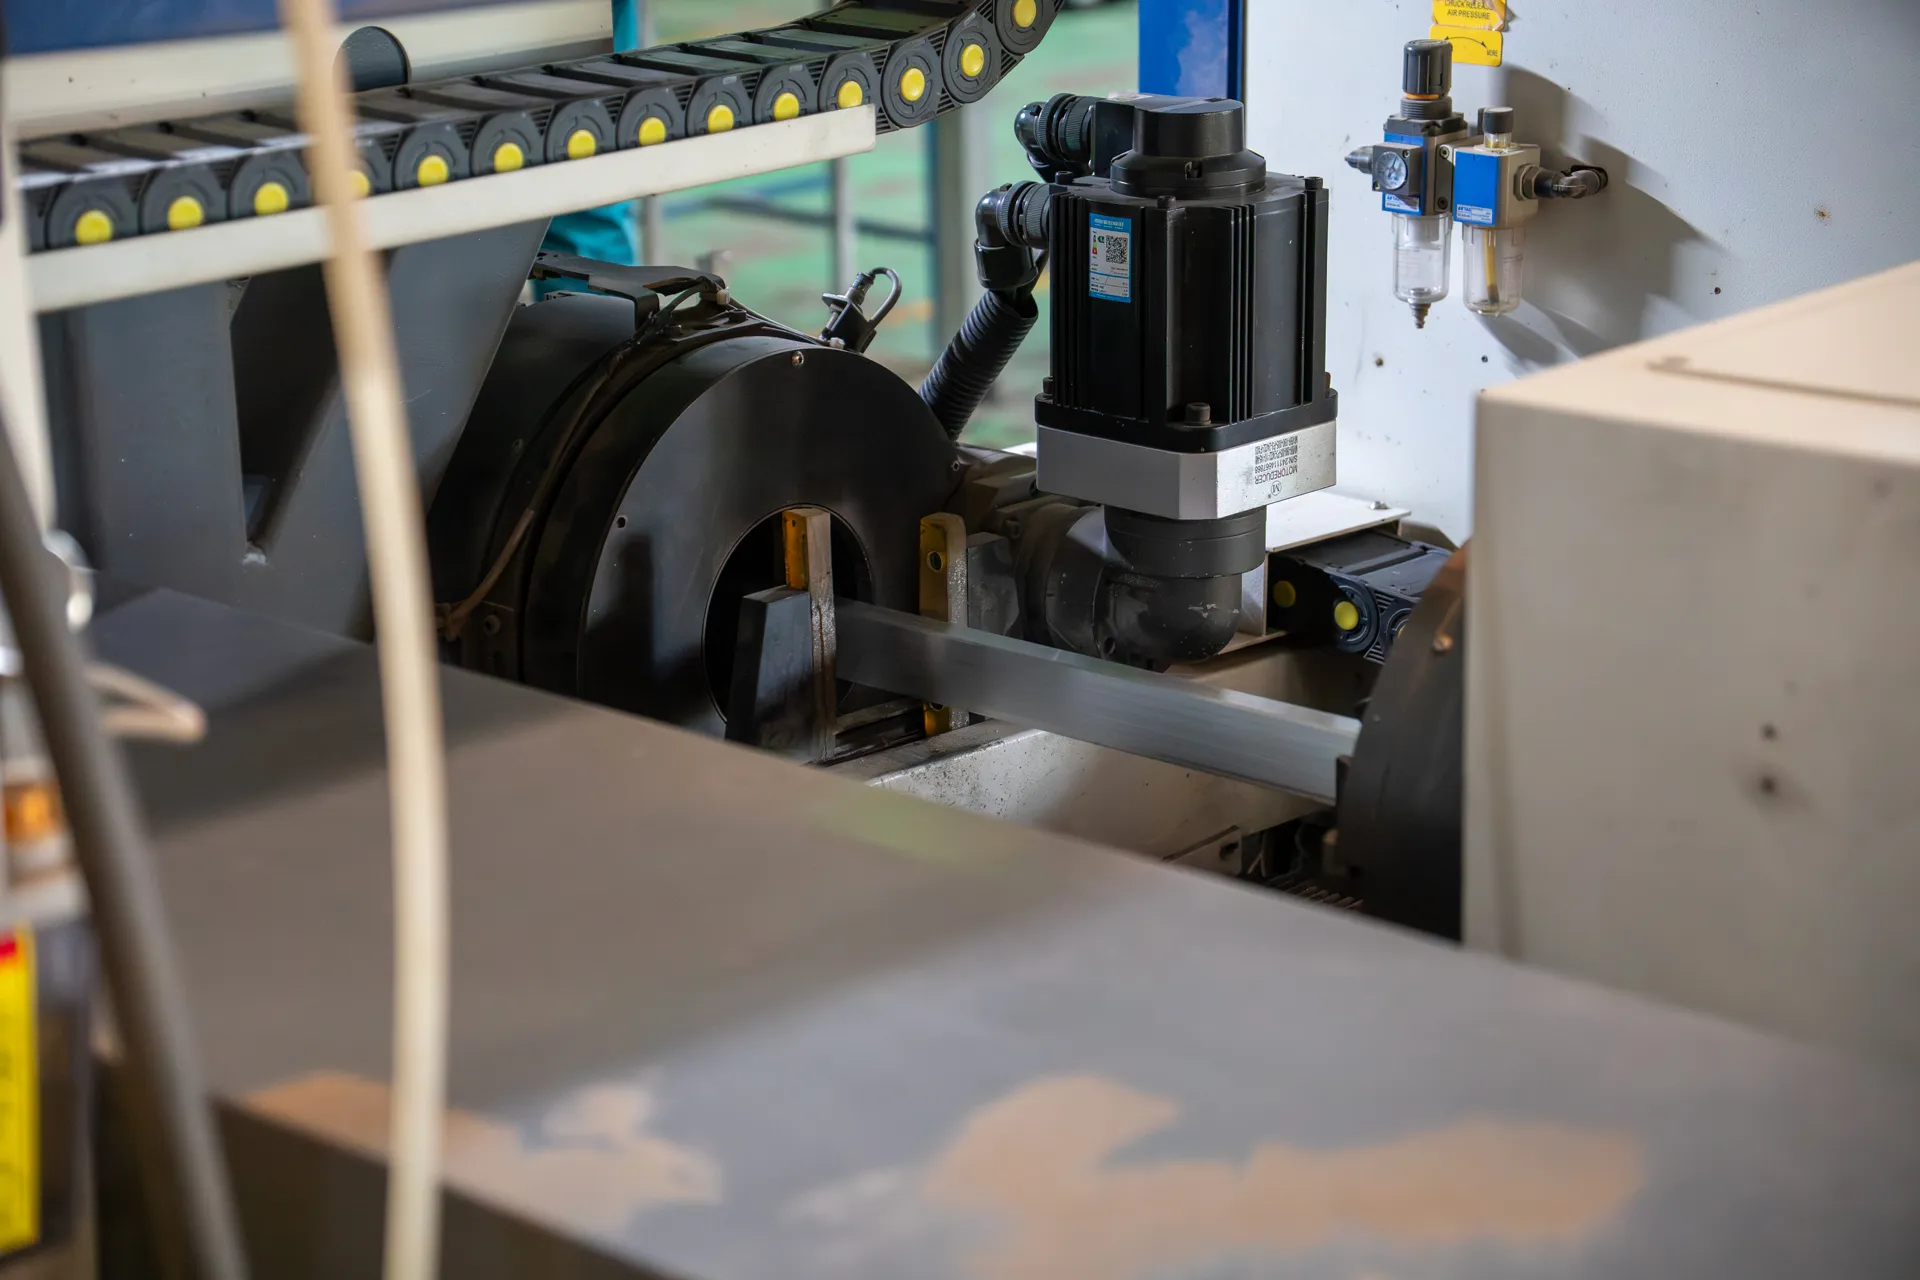
Fiber laser on profile and sheet, cutting notches, mitres and fixing holes in one operation so a joint is located by geometry rather than by a fitter’s eye.

Forming

±0.5° / ±0.3 mm

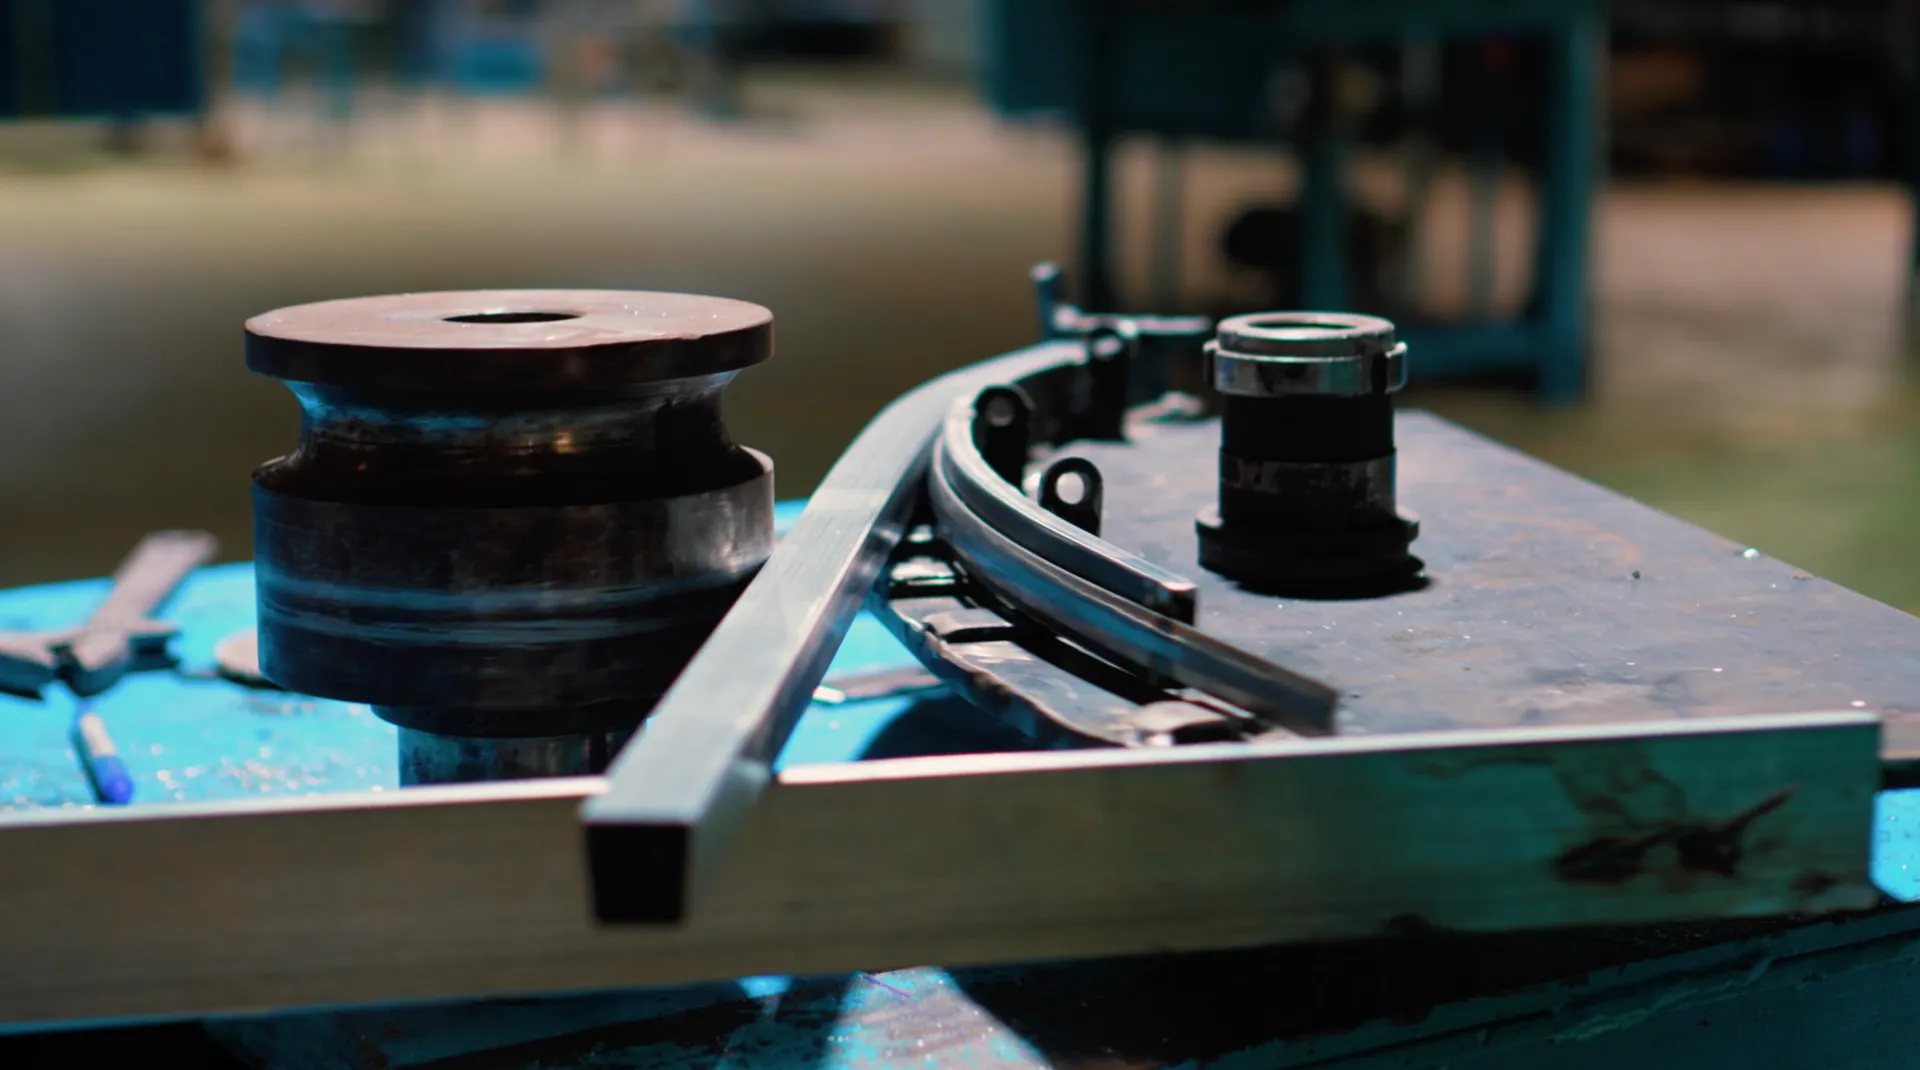
CNC press brake with programmable backgauge. Bend allowance and springback are compensated in the programme per alloy and thickness, so the first part off is within tolerance rather than the tenth.

Welding & Distortion Control

Fixtured, verified

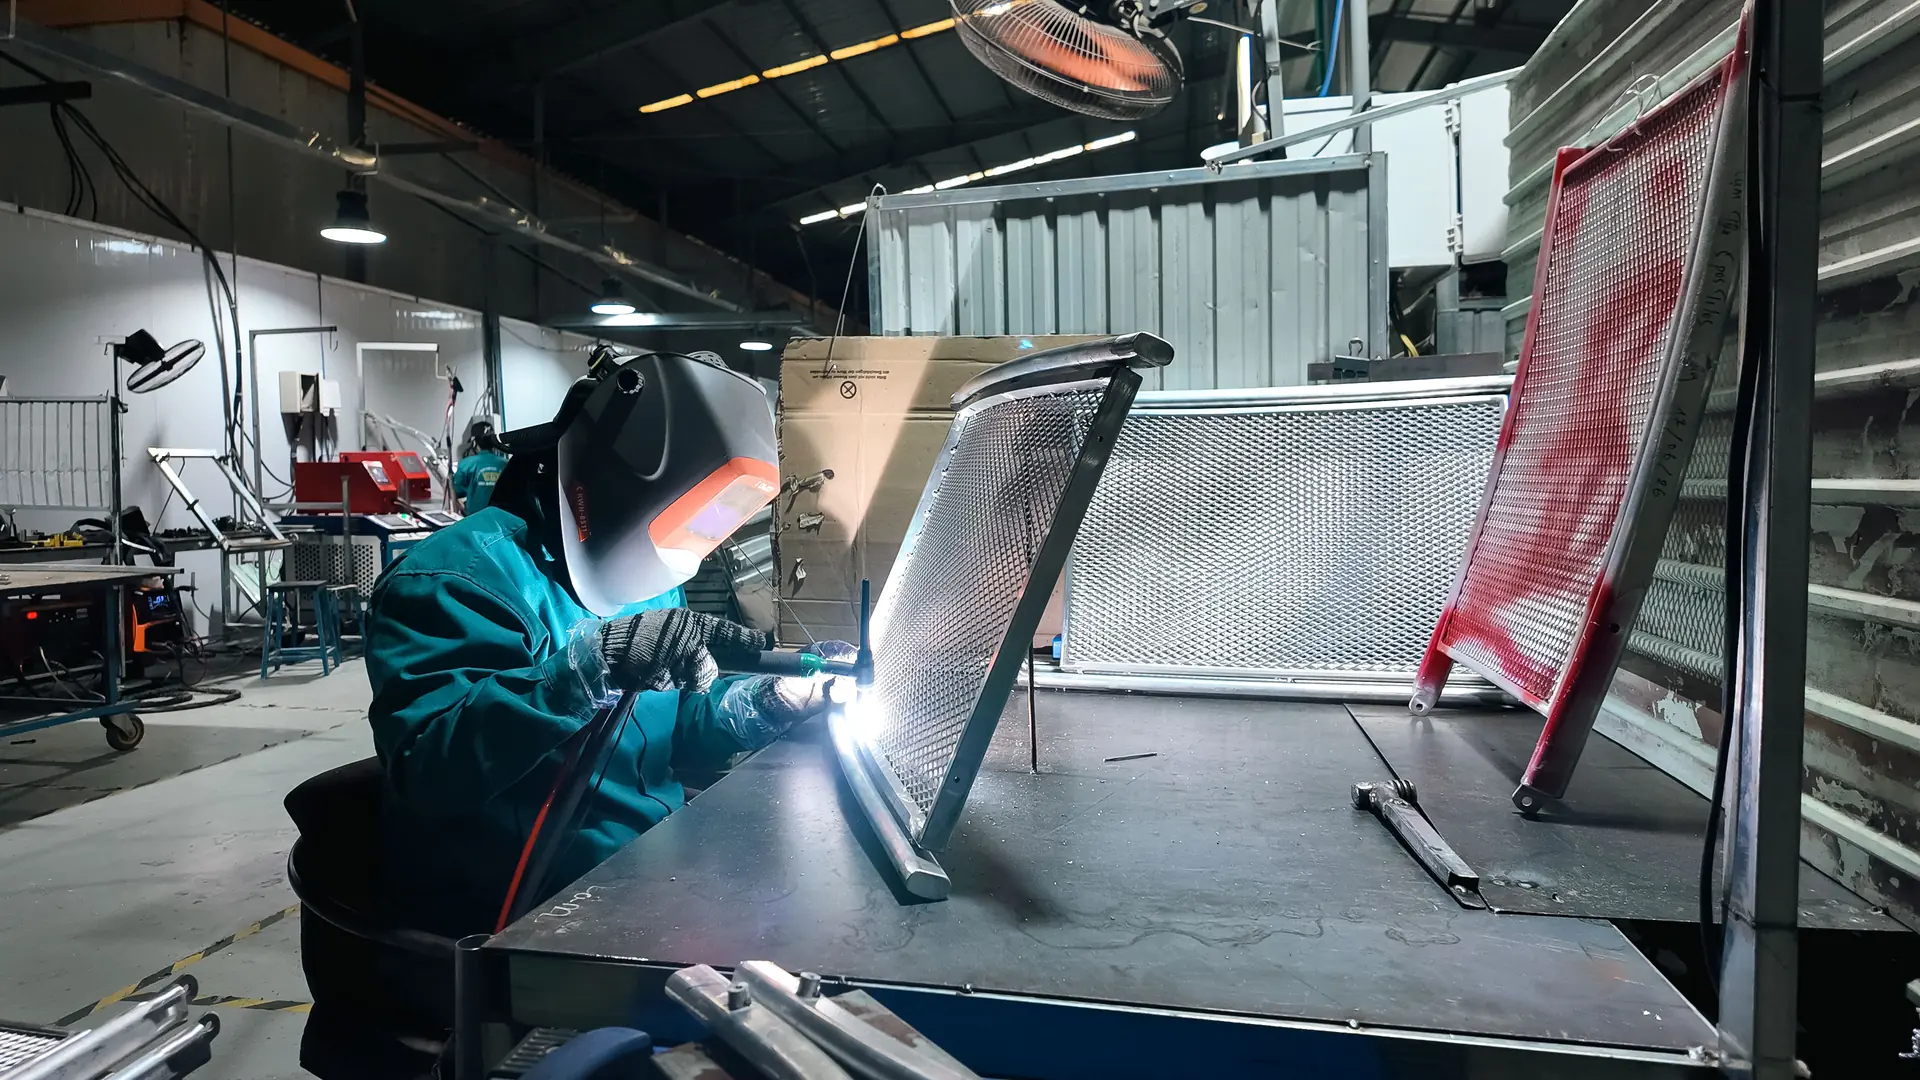
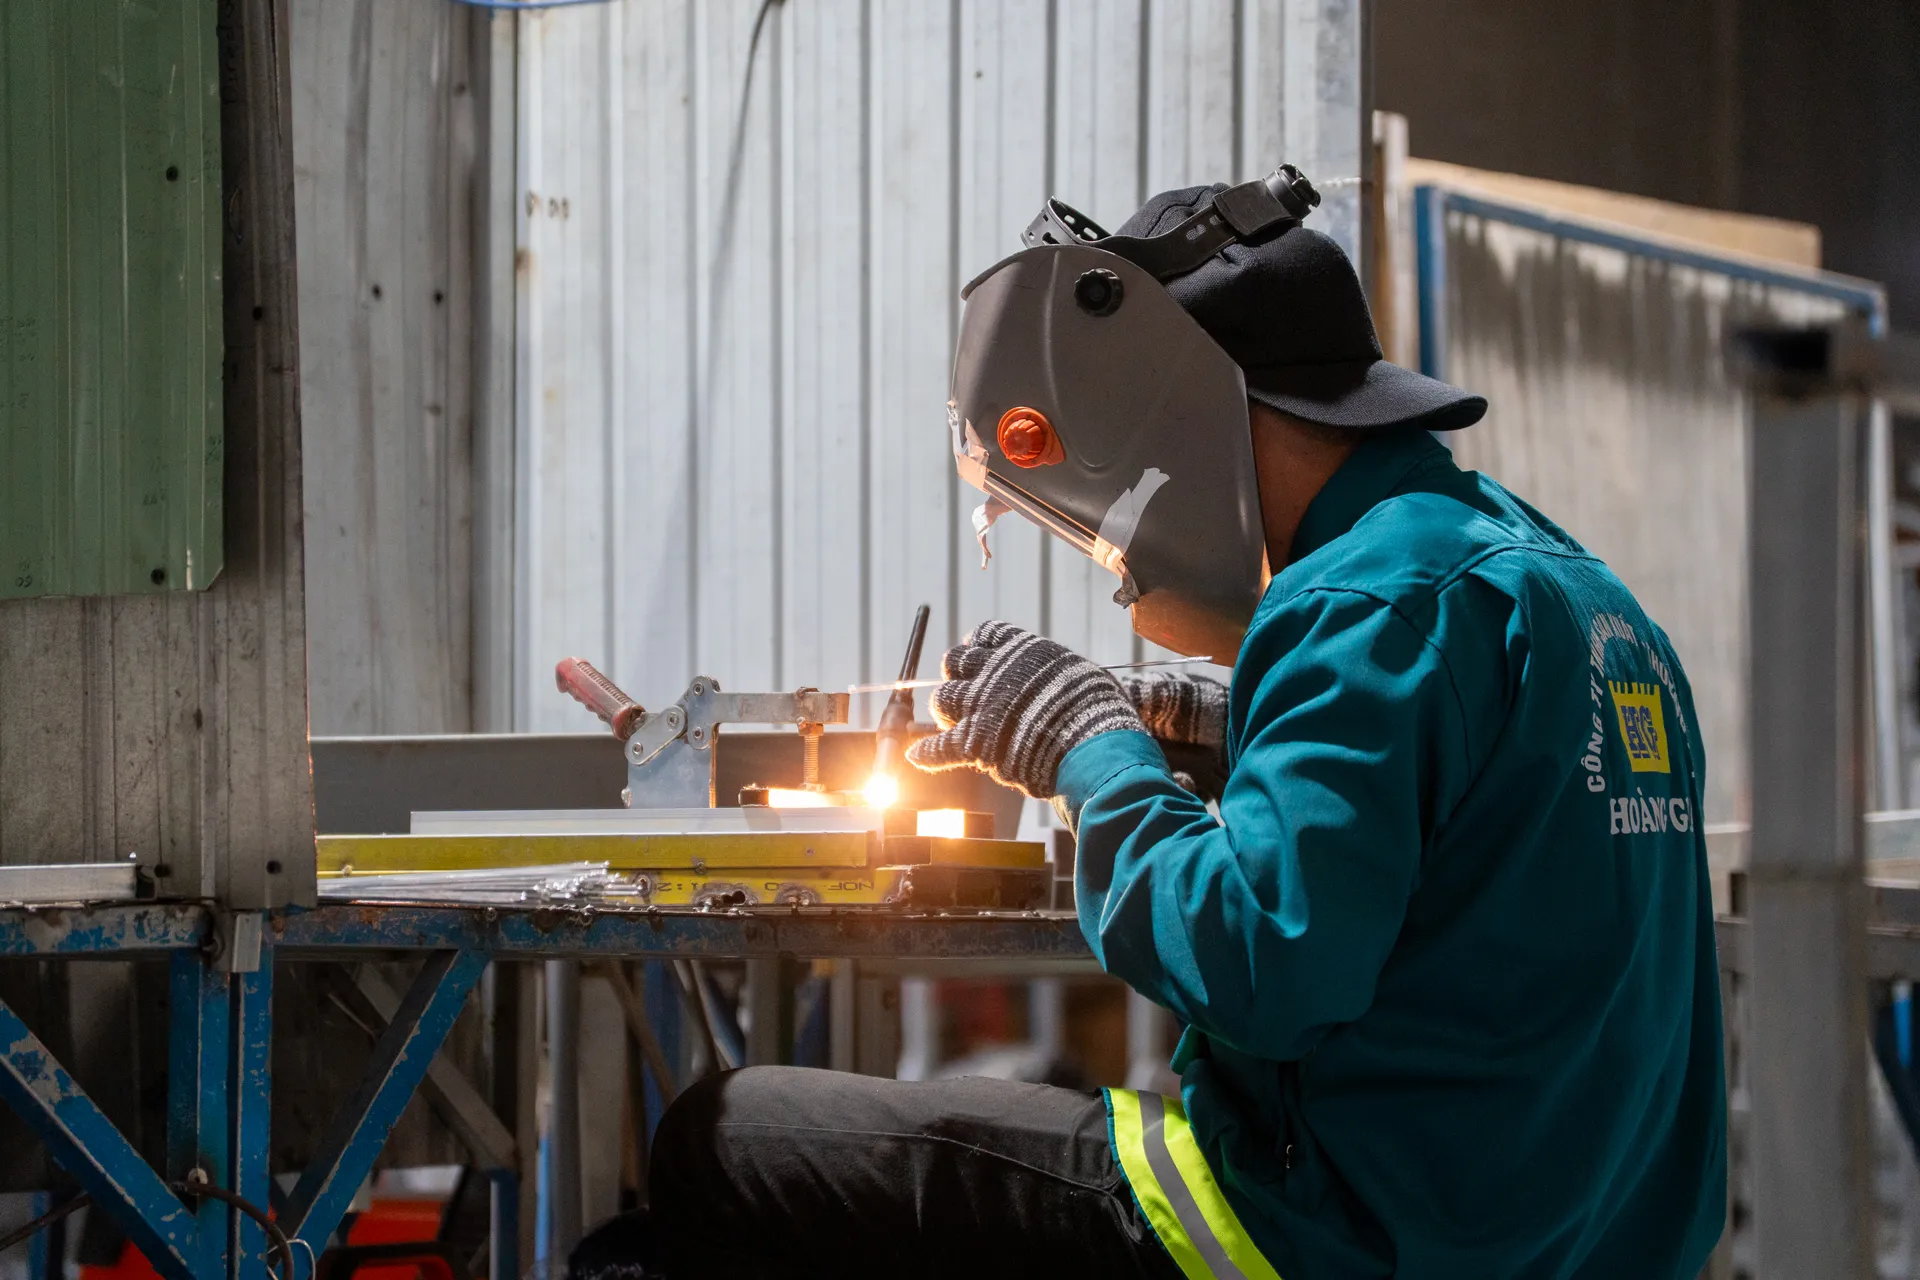
MIG and TIG in dedicated fixtures. Sequence, heat input and clamping are set to balance shrinkage across the frame, with staged release and post-weld checks. This is the step that separates factories.

Weld Dressing

By hand, inspected

Welds are ground and blended so the joint disappears under coating. On visible joins the target is a frame that reads as one continuous section.

THE CHAIN

Seven Steps From Billet
To Coated Frame

Section Design

Per programme

We draw our own extrusion profiles rather than buying stock tube. Wall thickness sits where the load is, and fixing points are extruded in rather than welded on — fewer welds, less distortion, a cleaner line.

Alloy & Certification

Per batch

6063-T5 as standard for frames, higher-strength alloys where a section is doing structural work. Every delivery arrives with a mill certificate and is verified before it enters the store.

Laser Cutting

±0.2 mm

Fiber laser on profile and sheet, cutting notches, mitres and fixing holes in one operation so a joint is located by geometry rather than by a fitter’s eye.

Forming

±0.5° / ±0.3 mm

CNC press brake with programmable backgauge. Bend allowance and springback are compensated in the programme per alloy and thickness, so the first part off is within tolerance rather than the tenth.

What We Work

METAL GRADE JOINING FINISH TYPICAL USE
Aluminium 6063-T5 MIG / TIG, fixtured Polyester powder All frames, dining, lounge, loungers
Aluminium, structural 6061 on request TIG Polyester powder Long spans, canopy and daybed frames
Stainless steel 304 TIG, back-purged Brushed or electropolished Premium dining, marine-adjacent
Stainless steel 316 / A4 TIG, back-purged Brushed Coastal and poolside; all fasteners
Carbon steel To drawing MIG Galvanised then powder Sheltered and structural applications