

METALWORK
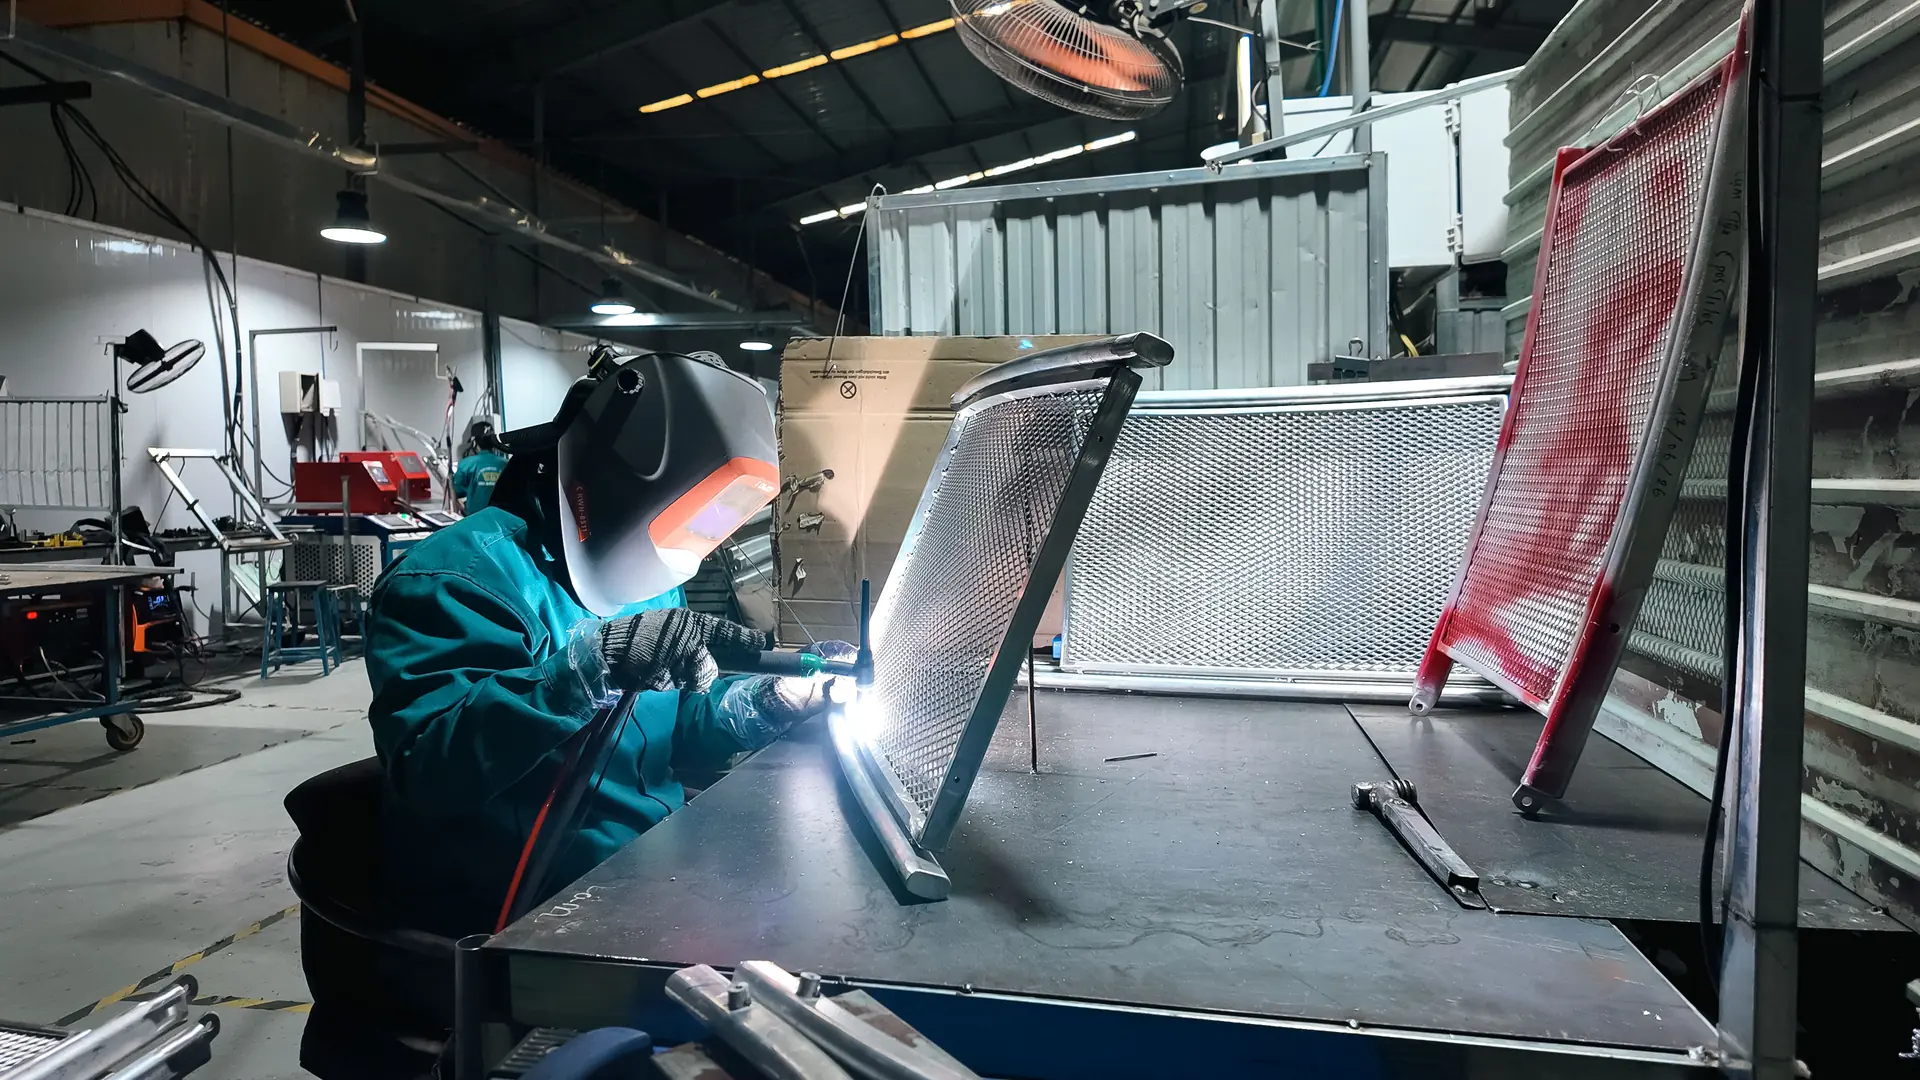
Aluminium is unforgiving. It conducts heat away faster than steel, so a weld that looks sound can be cold; it moves as it cools, so a frame that measured true in the fixture can leave it out of square; and it shows every ripple once a gloss coat goes over the top.
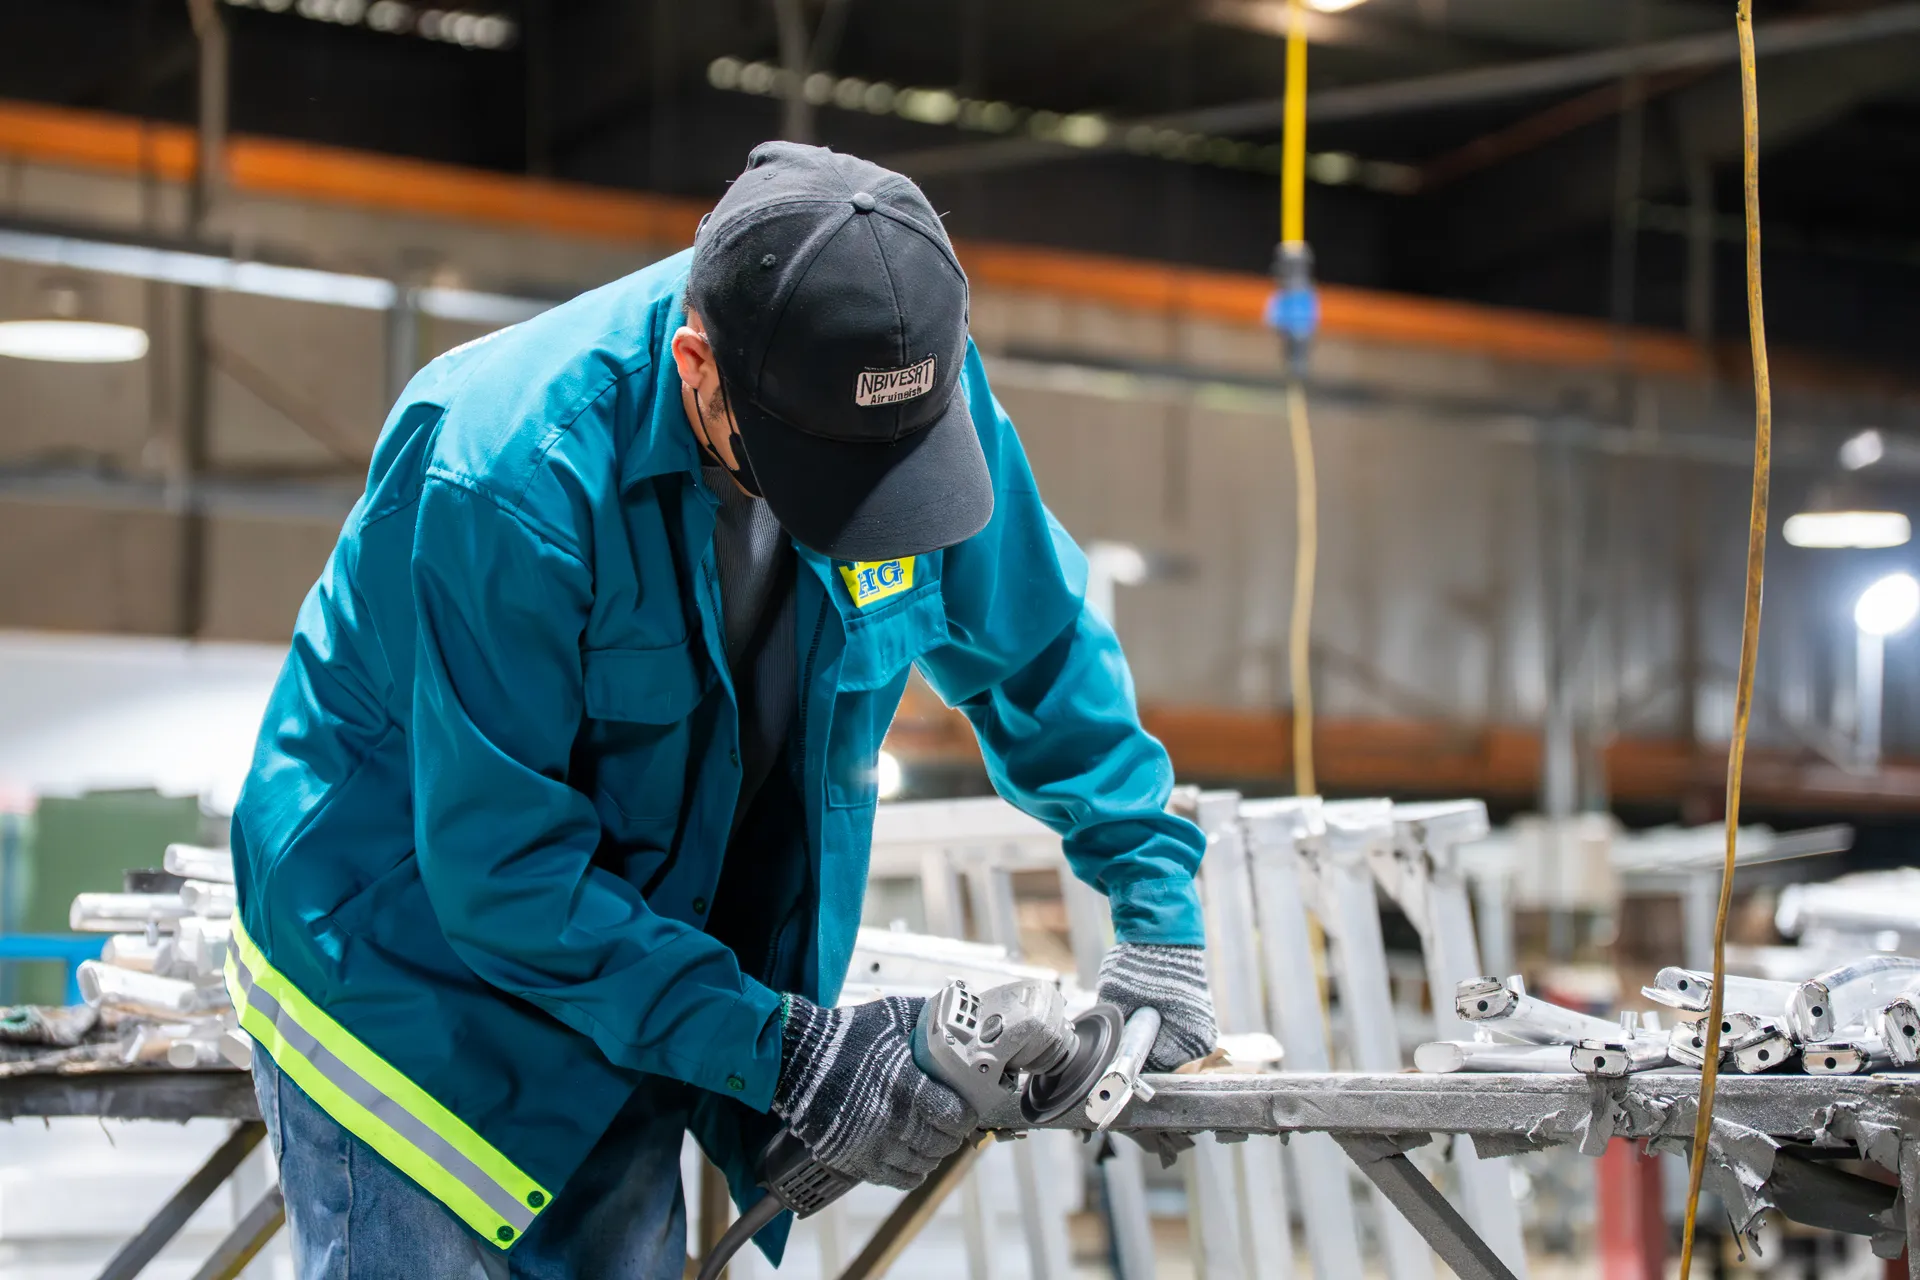
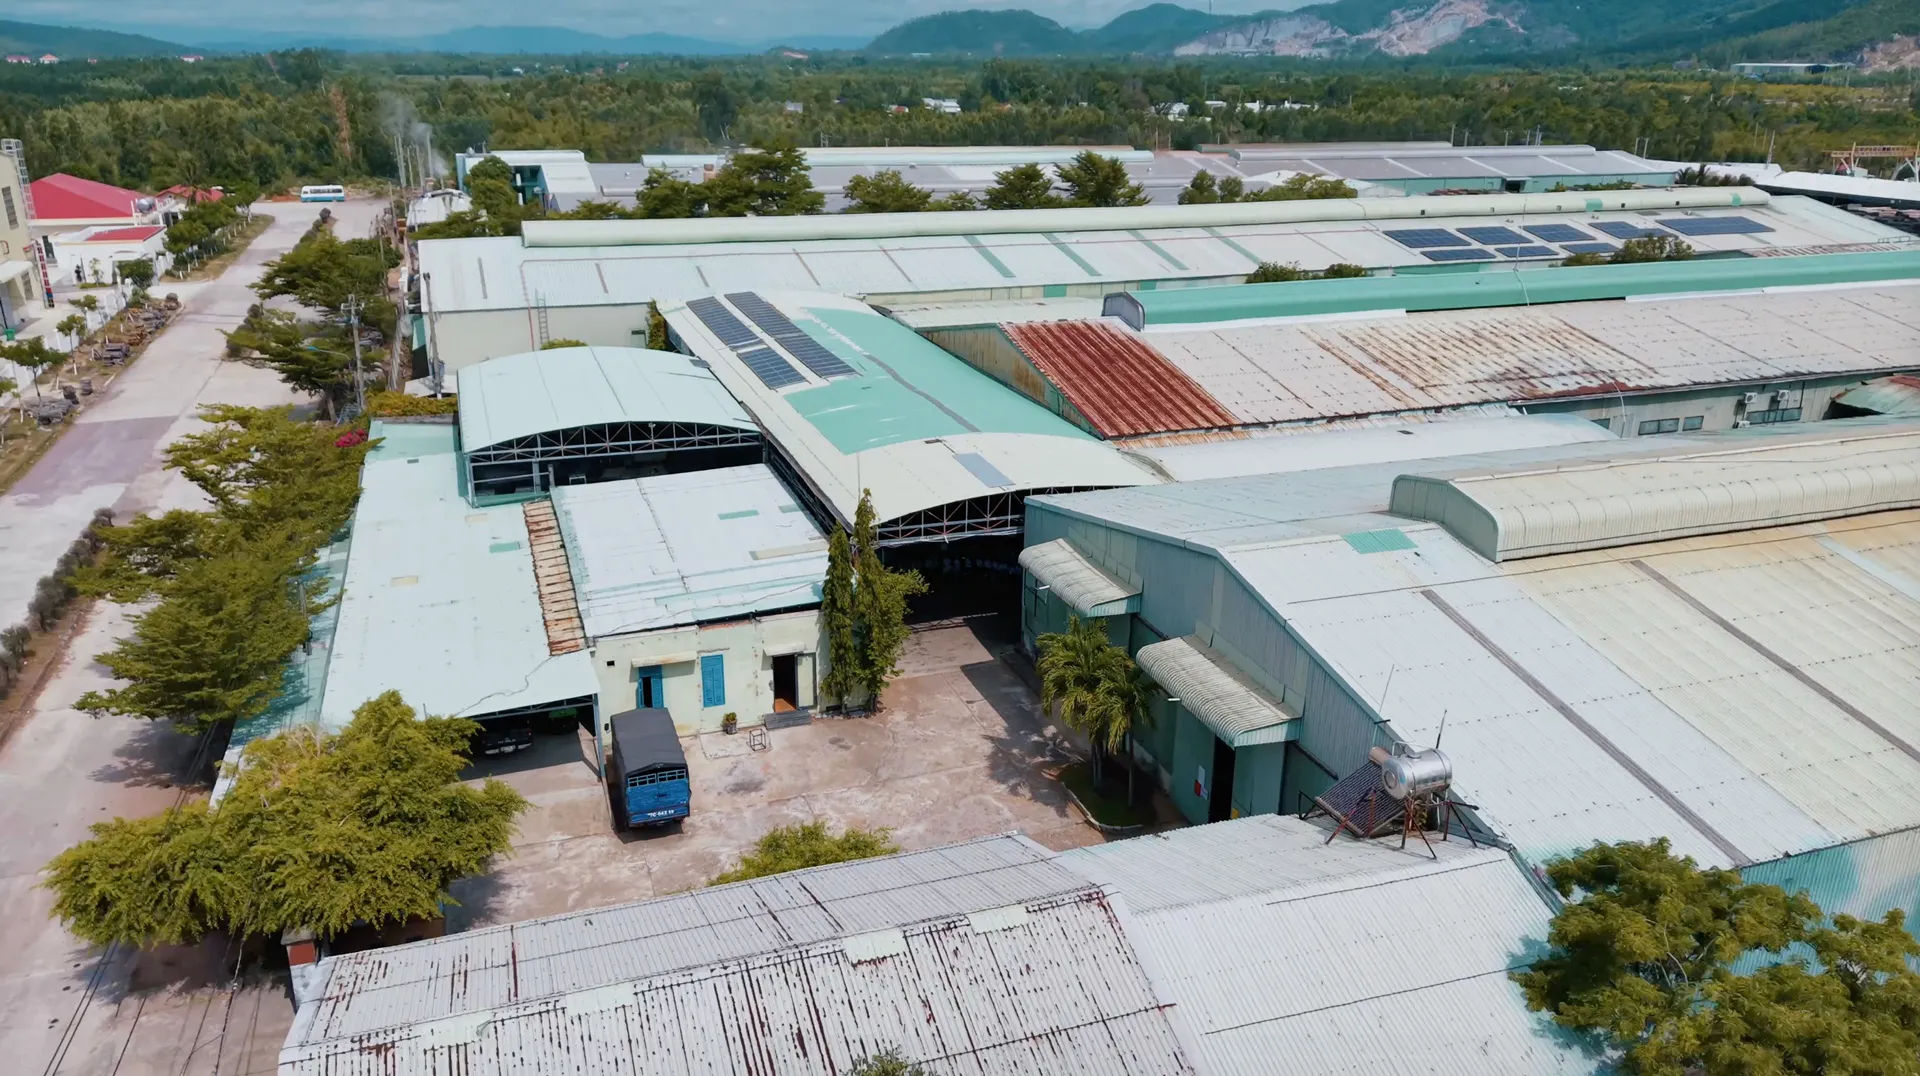
Our Mechanical Division is staffed with craftsmen who have spent years on the precise fabrication of steel, aluminium and stainless frames. The processes below are ordinary; holding them together across a long run is not.
THE CHAIN
Per programme


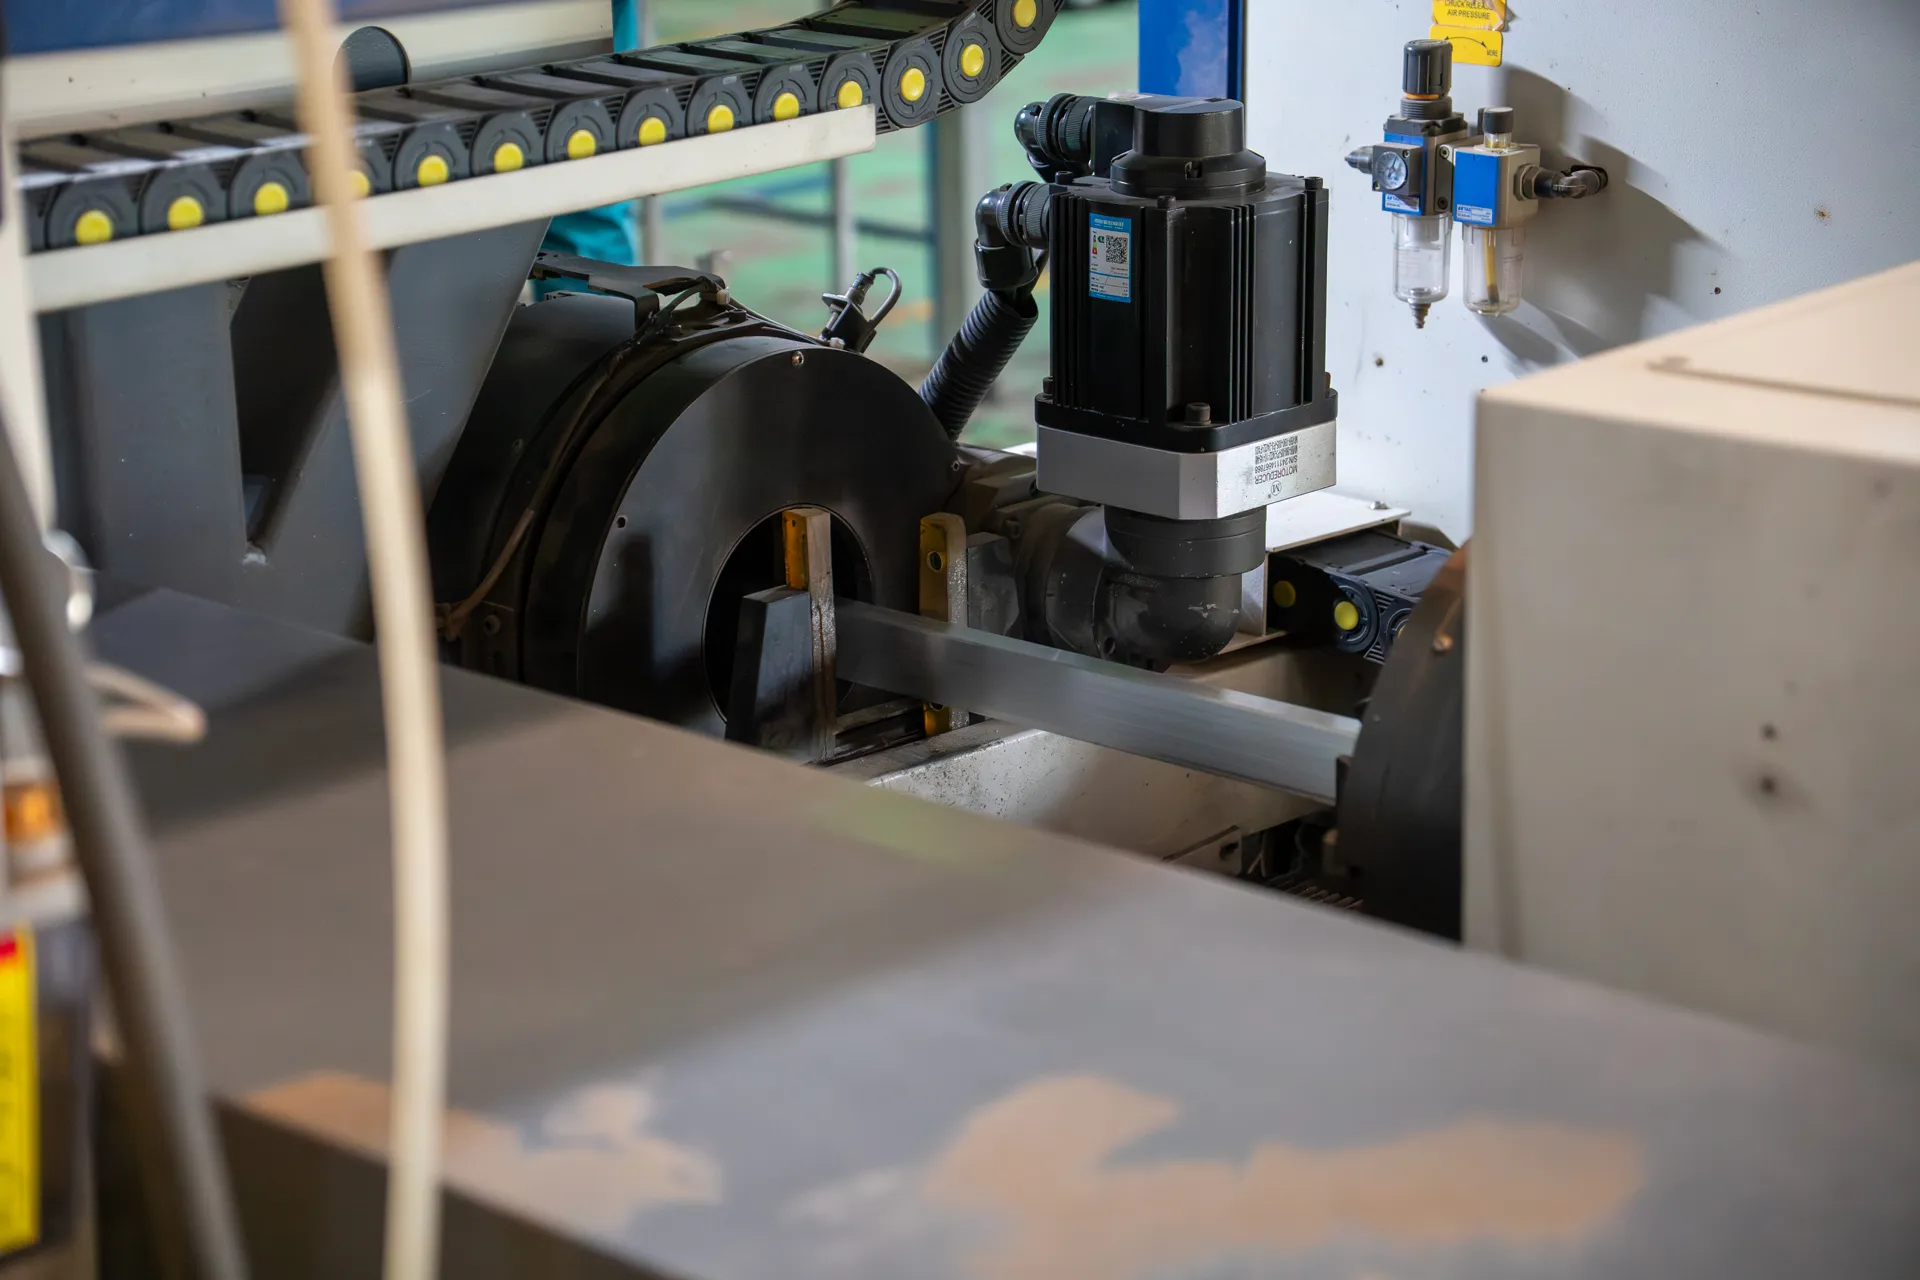
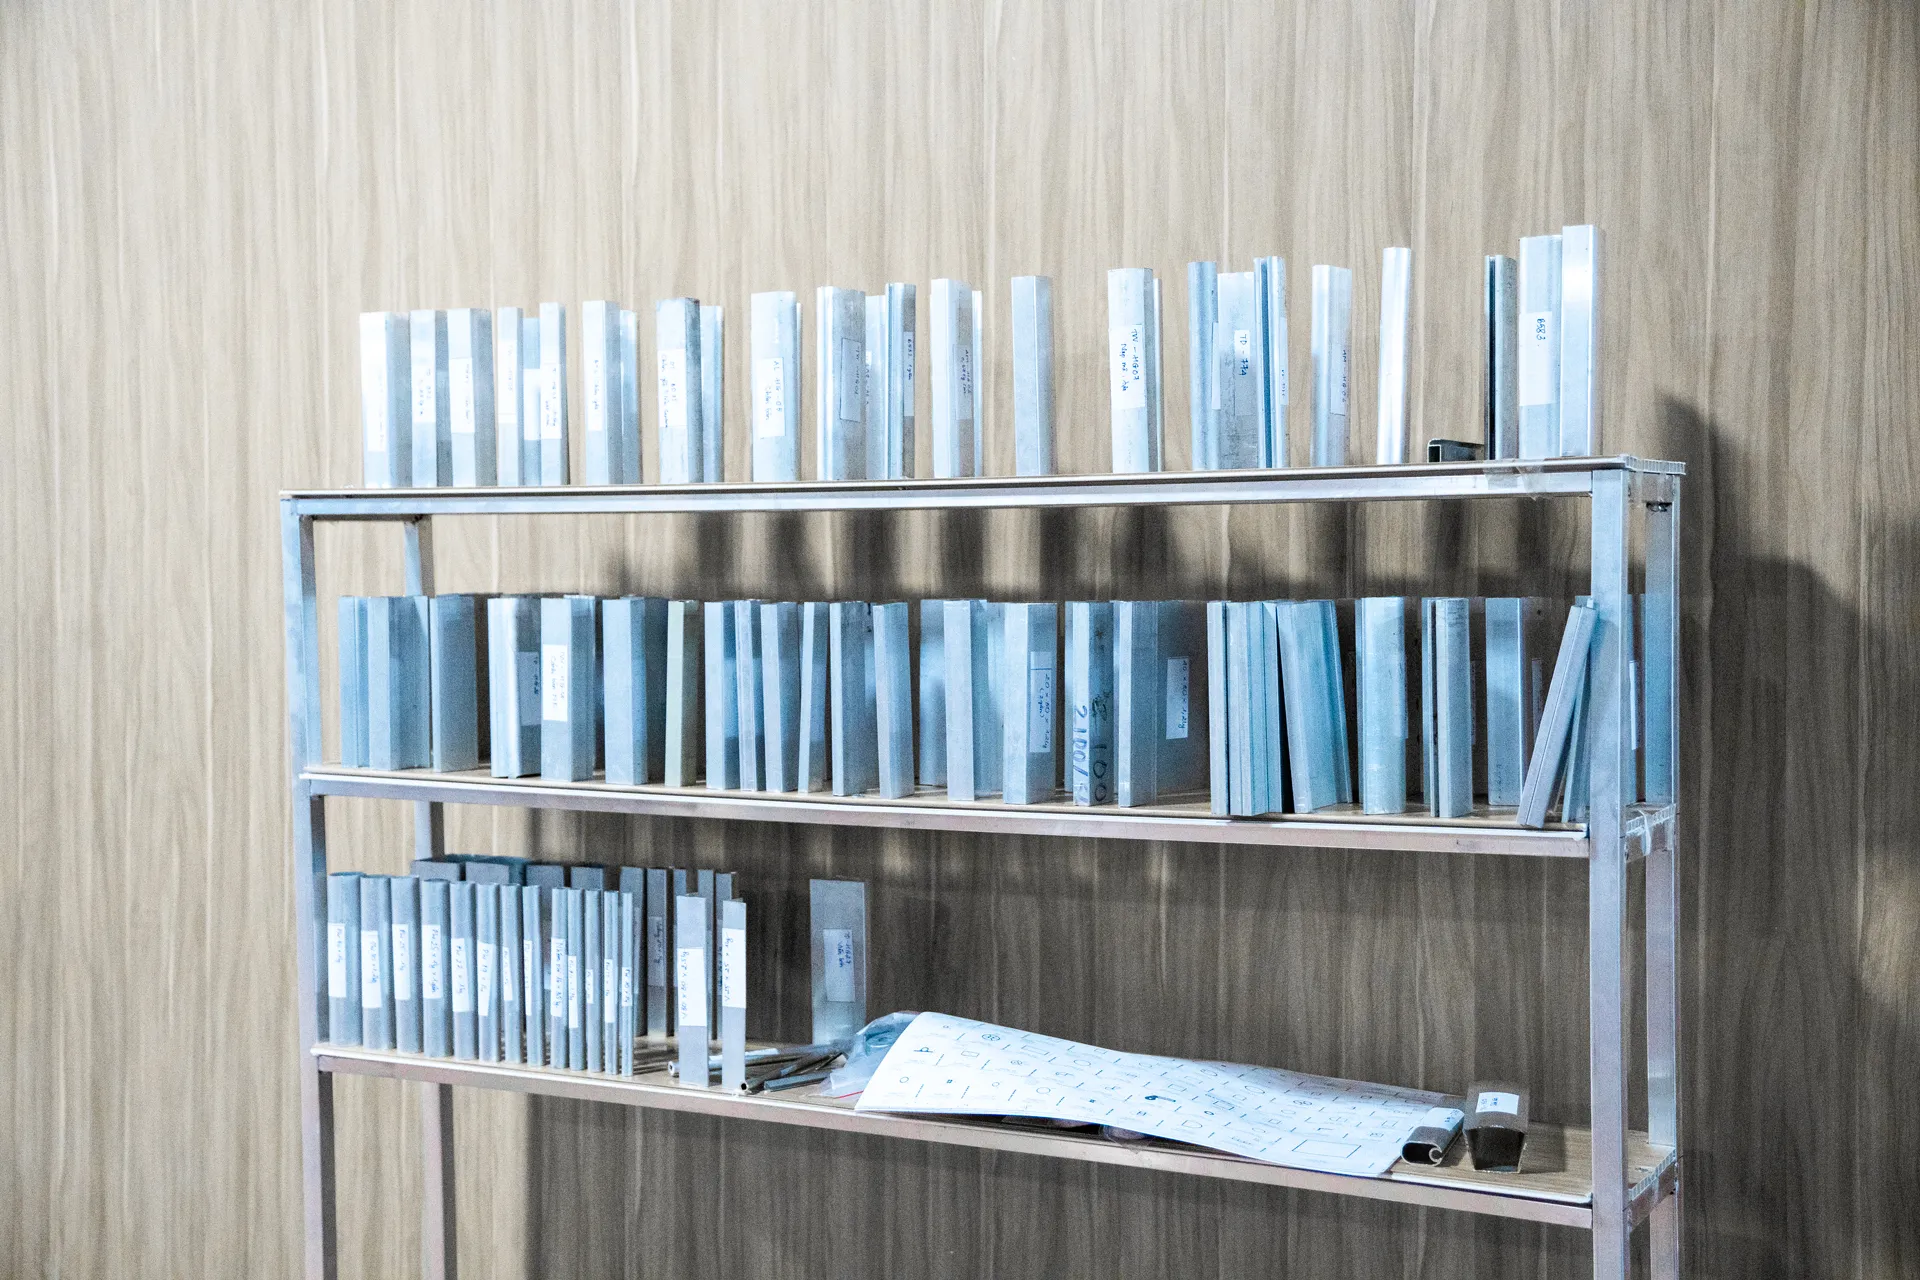
We draw our own extrusion profiles rather than buying stock tube. Wall thickness sits where the load is, and fixing points are extruded in rather than welded on — fewer welds, less distortion, a cleaner line.
Per batch

6063-T5 as standard for frames, higher-strength alloys where a section is doing structural work. Every delivery arrives with a mill certificate and is verified before it enters the store.
±0.2 mm

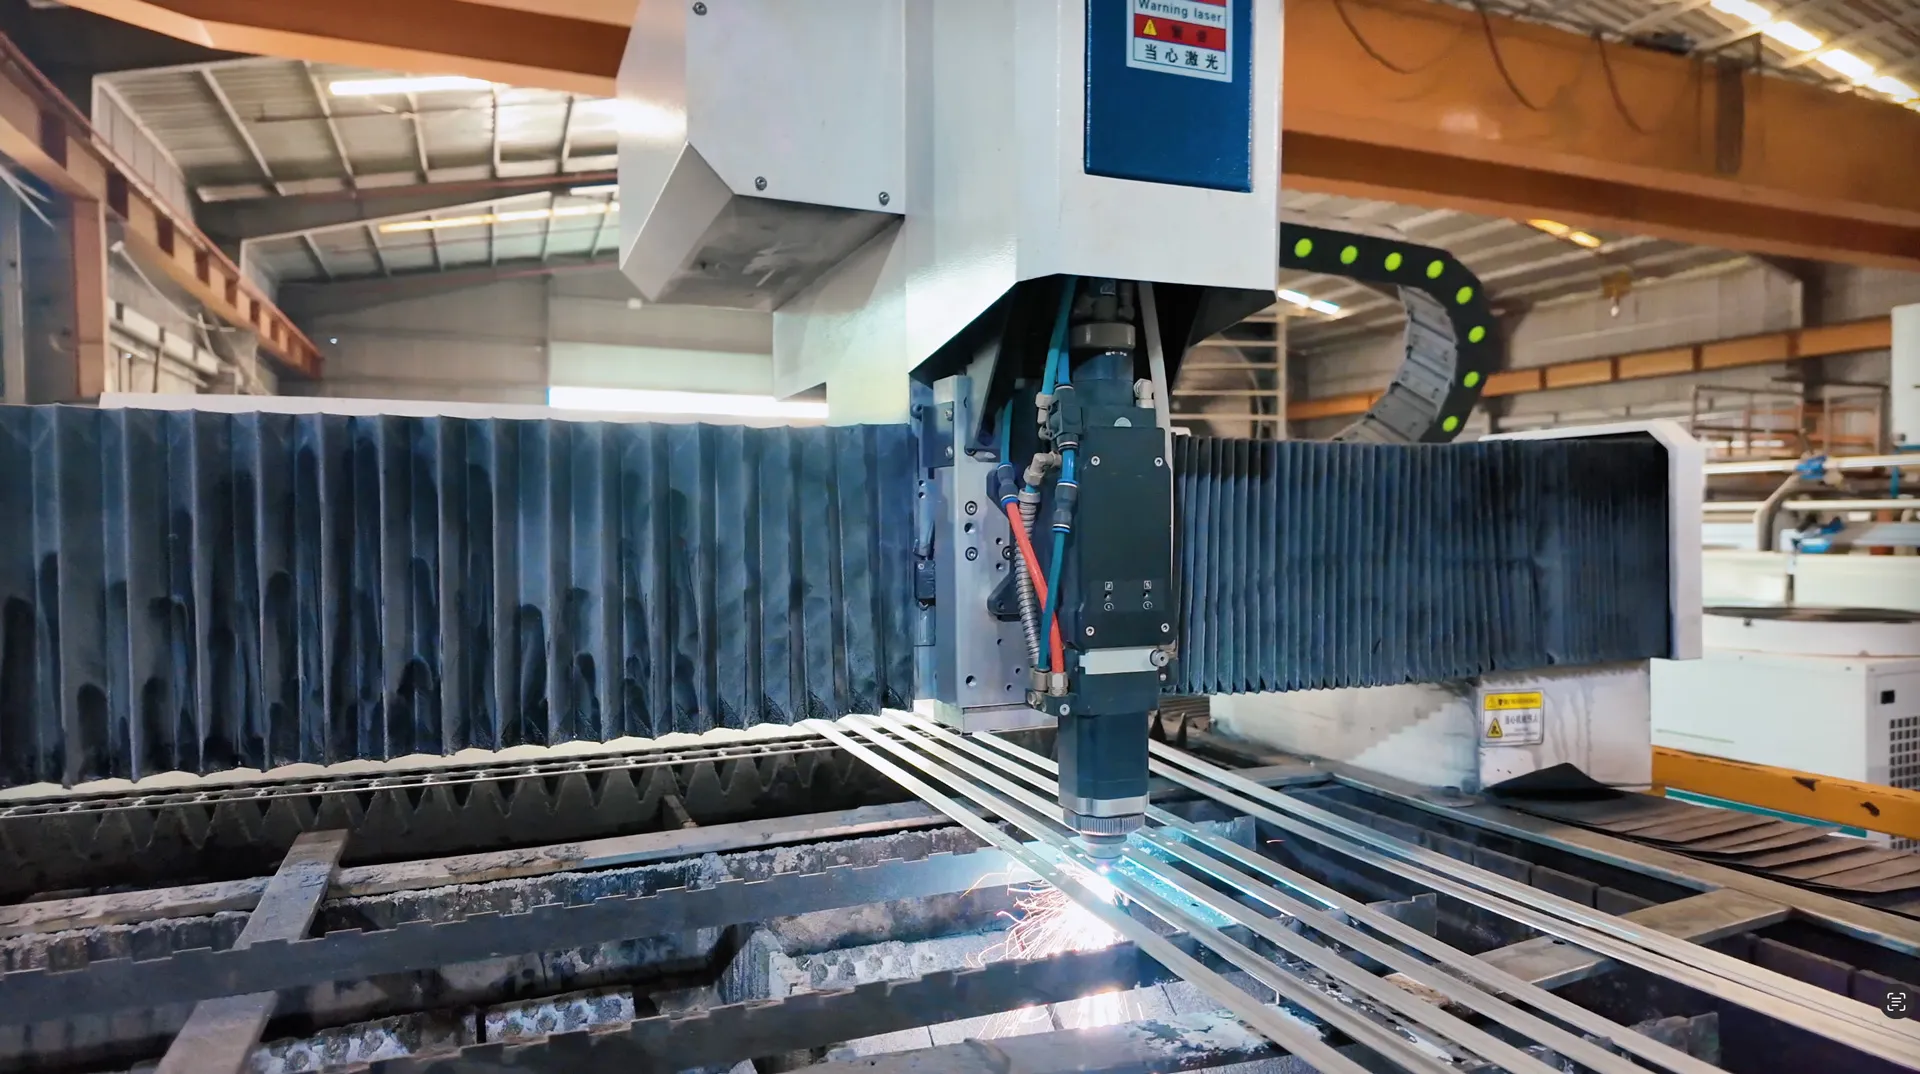
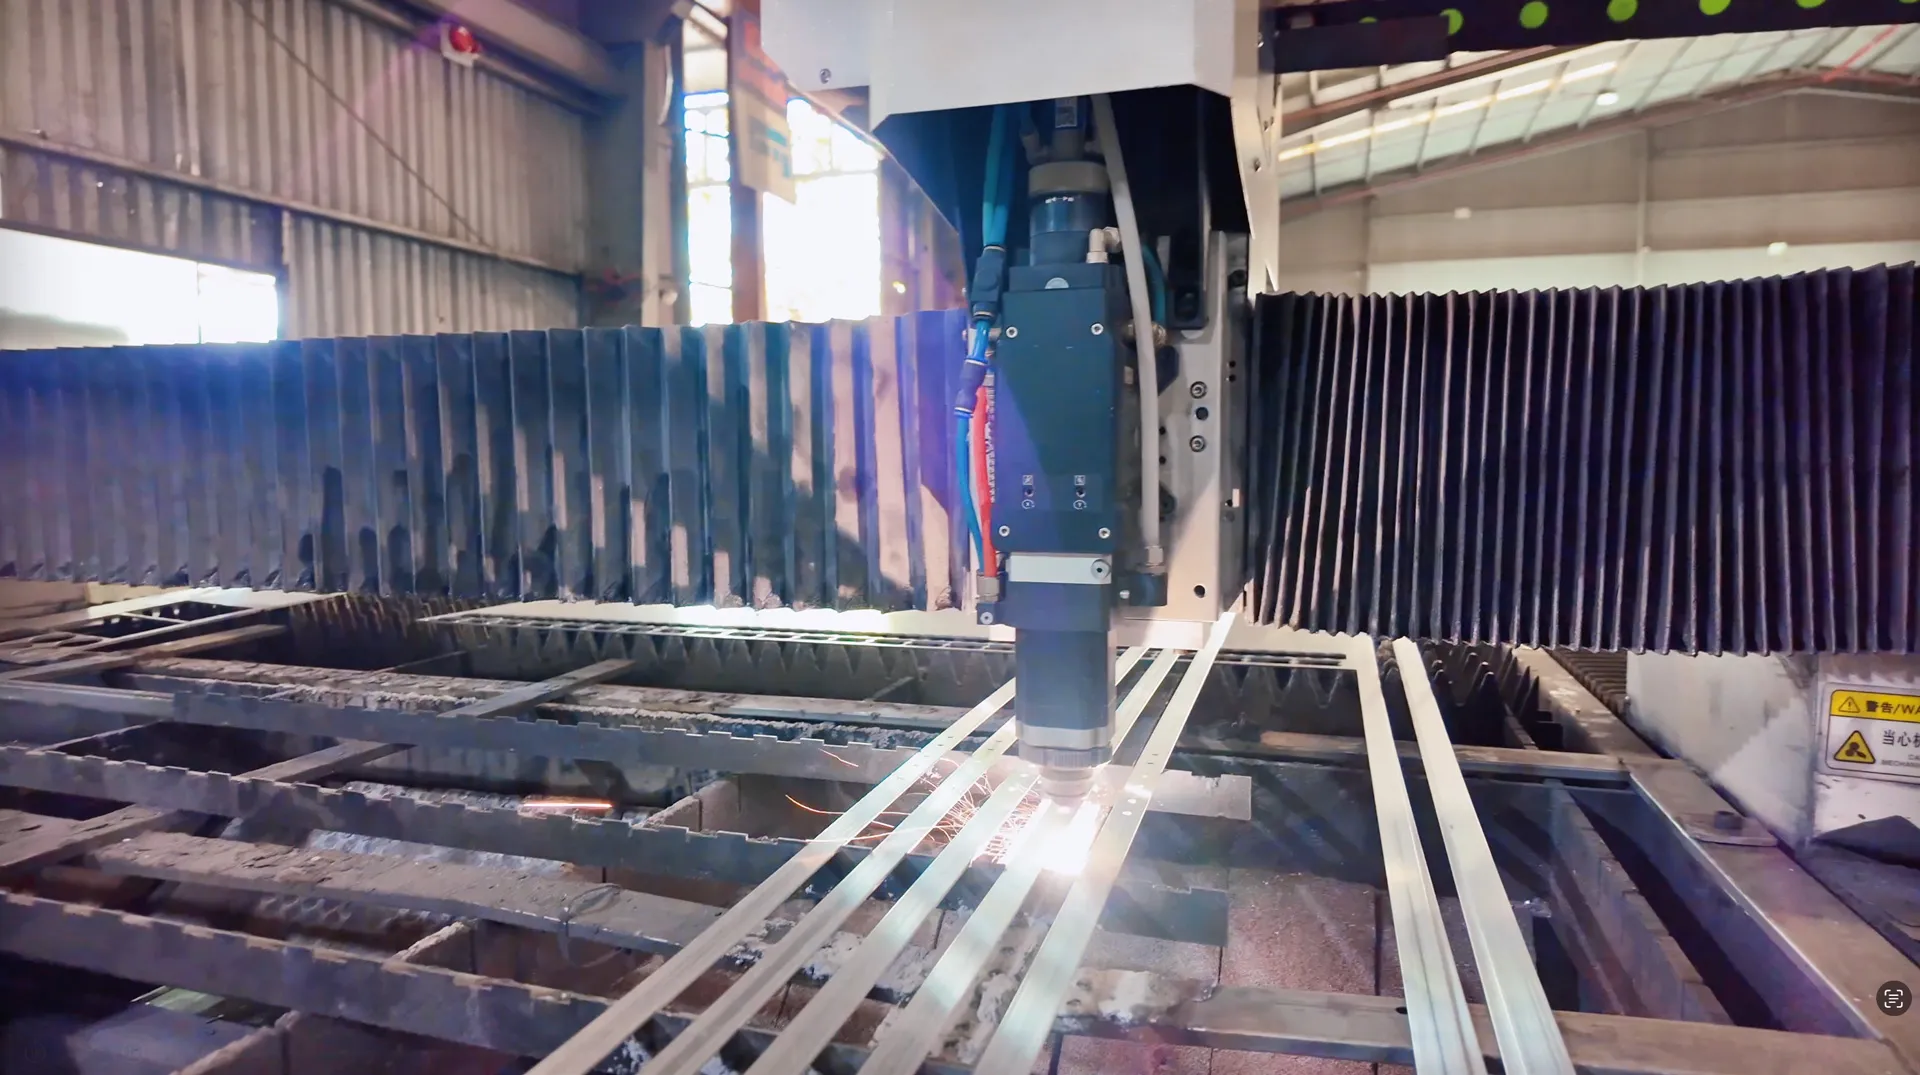
Fiber laser on profile and sheet, cutting notches, mitres and fixing holes in one operation so a joint is located by geometry rather than by a fitter’s eye.
±0.5° / ±0.3 mm

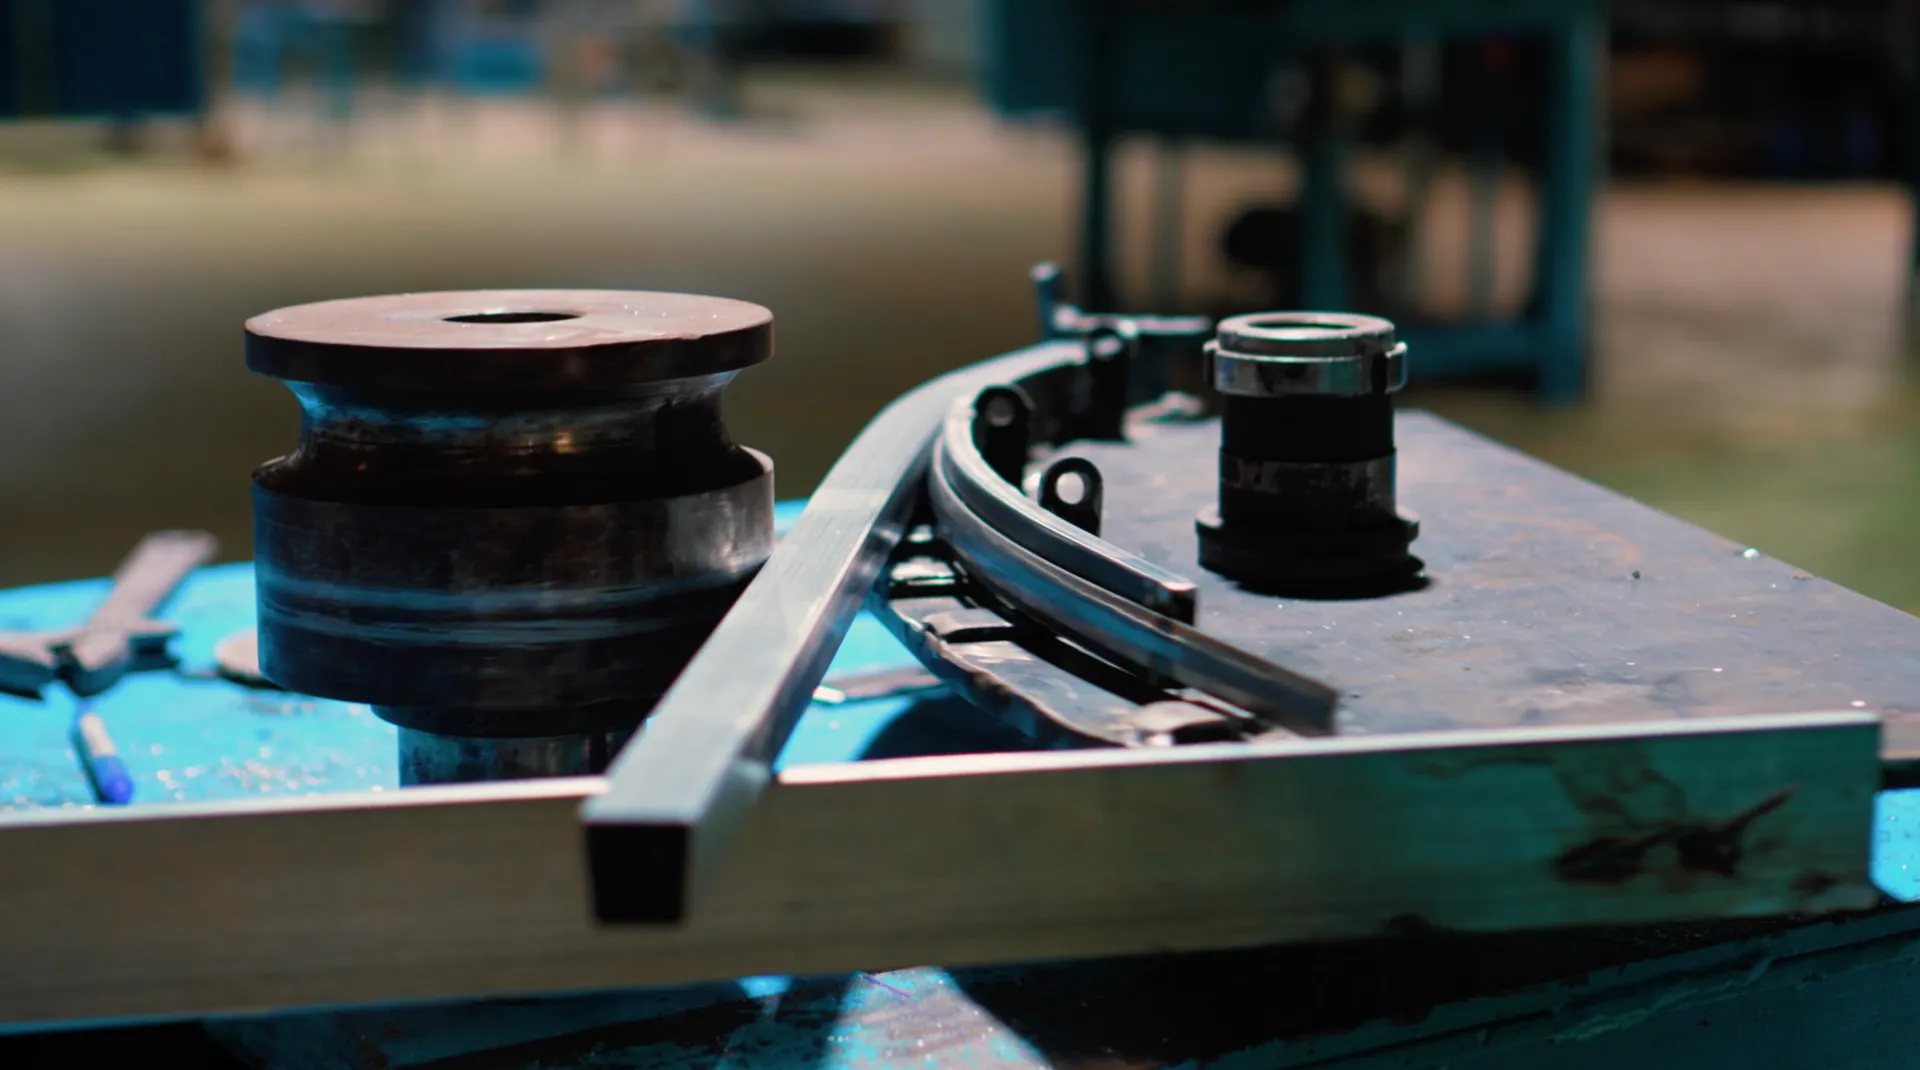
CNC press brake with programmable backgauge. Bend allowance and springback are compensated in the programme per alloy and thickness, so the first part off is within tolerance rather than the tenth.
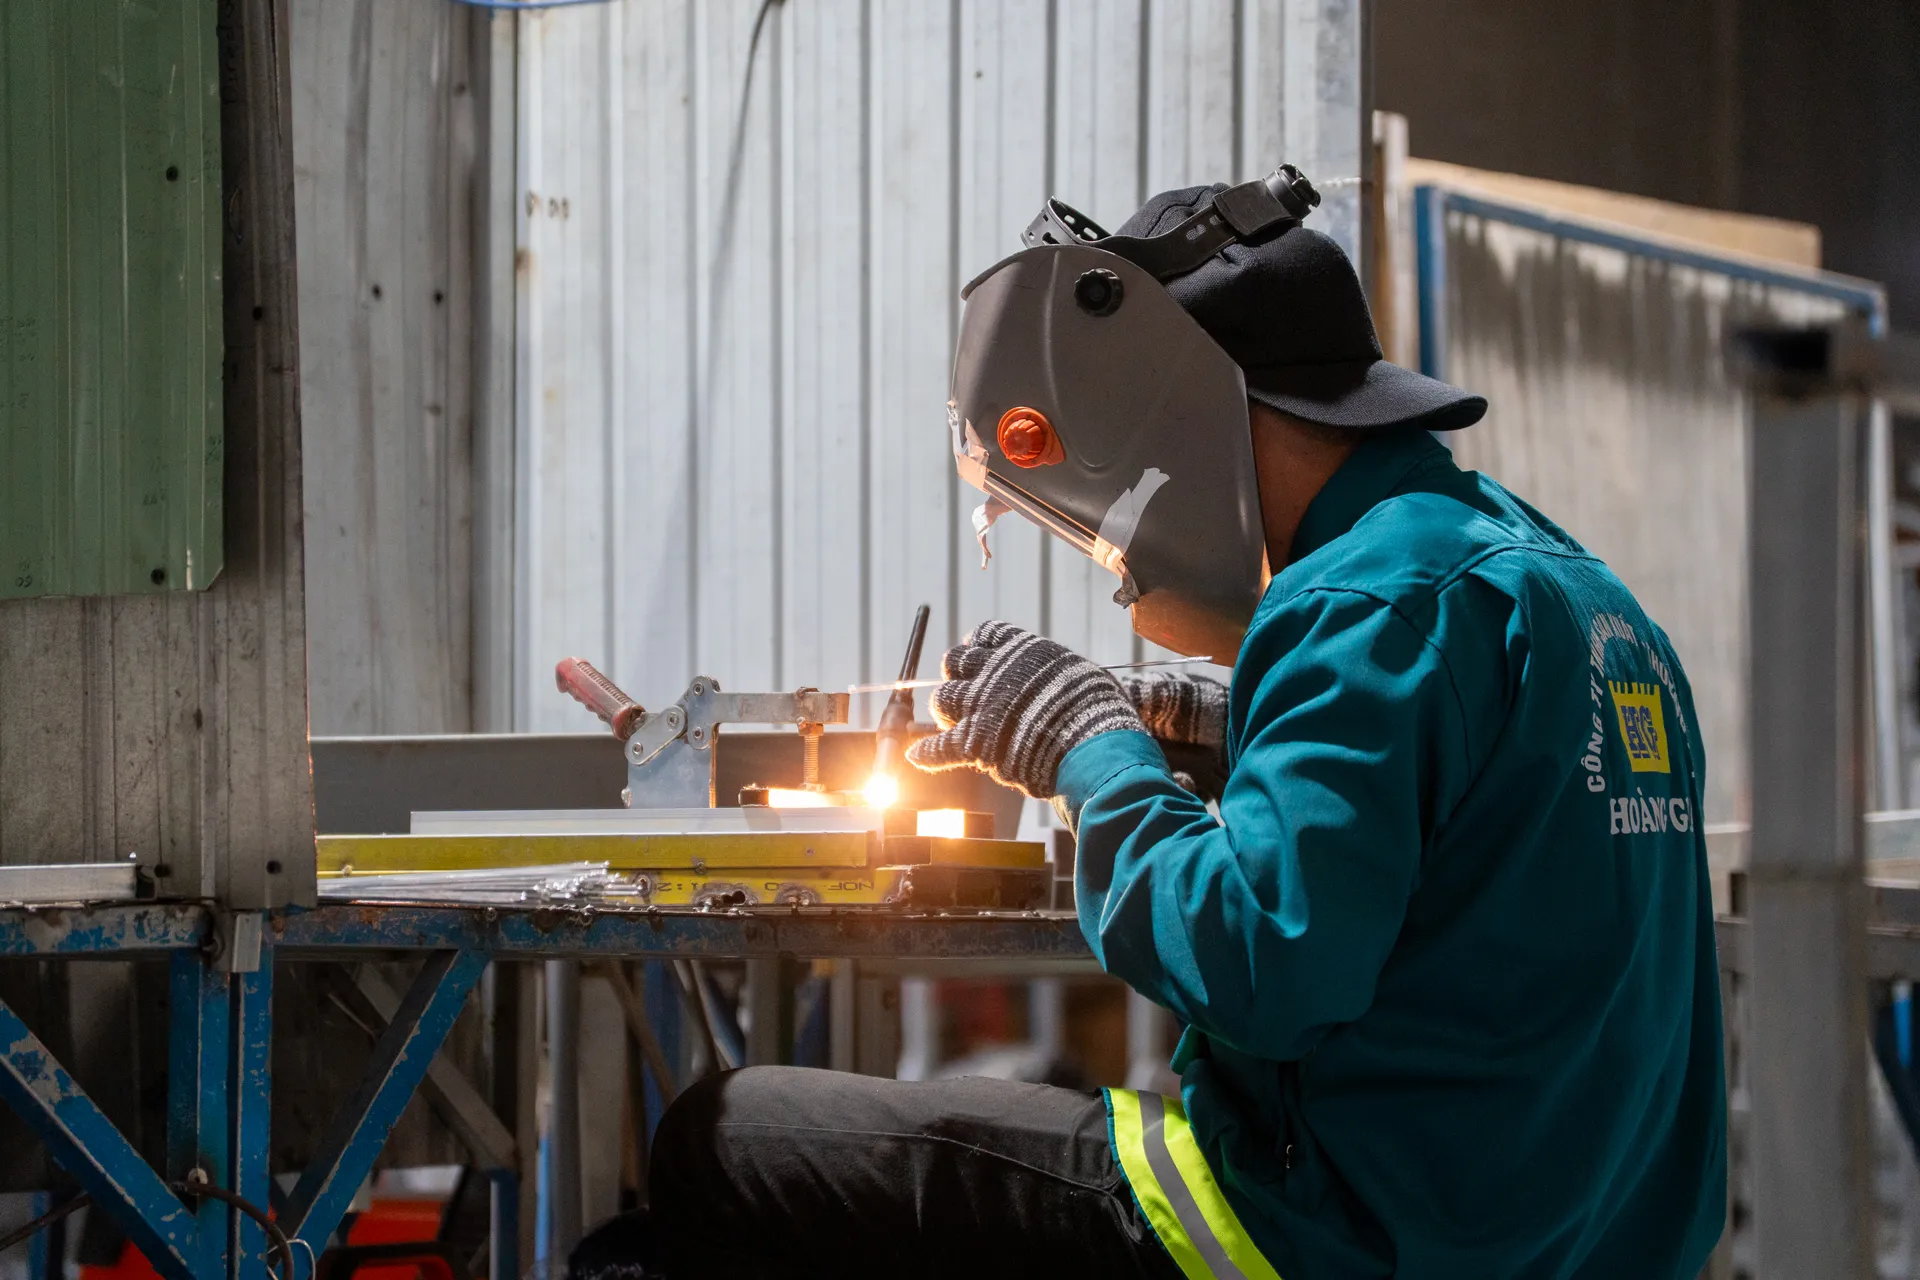

A single cut holding ±0.2 mm means little if the stack across a welded frame is uncontrolled. We fixture to one datum from laser through to assembly, and measure the assembly rather than the part.

Powder thickness is the visible number; pre-treatment is the one that matters. Bath chemistry and stage control are logged, and salt-spray results are quoted against the actual system rather than a supplier’s brochure.

Rope terminations, weave anchors, sling battens, slat fixings and cushion clips are all designed into the extrusion, not added afterwards. It is why our mixed-material pieces do not rattle.